Engineered for extreme thermal resistance, anatomical comfort, and high-performance weather protection. Custom manufactured to your brand's exact tech specs.
By integrating technical weaving, RDS-certified insulation sourcing, automated CAD pattern grading, and certified CE testing under a single family-owned infrastructure, we eliminate third-party commission markups while providing full transparency from yarn procurement to door-to-door shipping.
Procuring commercial and industrial winter overcoats for global distribution requires strict adherence to European Union conformity standards. A true CE Certified Winter Overcoats Factory does not merely assemble fabric panels; it engineers complete thermal insulation systems verified under standards such as EN 342:2017 (Ensembles and garments for protection against cold) and EN 14058:2017 (Single garments for protection against cool environments).
To comply with these rigid benchmarks, our technical manufacturing floor focuses on three primary physical parameters:
| Standard / Norm | Key Testing Parameter | Factory Compliance Level | Commercial Application |
|---|---|---|---|
| EN 342:2017 | Thermal Insulation & Air Permeability | Class 3 Air Permeability / $I_{cler} > 0.310$ | Heavy Duty Cold Storage & Extreme Sub-Zero Outerwear |
| EN 14058:2017 | Thermal Resistance ($R_{ct}$) | Class 3 ($R_{ct} > 0.25\text{ m}^2\cdot\text{K/W}$) | Urban Executive Overcoats & Moderate Winter Outerwear |
| EN 343:2019 | Waterproofness & Water Vapour Resistance | Class 4:4 (Highest Hydrostatic & Breathability) | Tactical Snow & Weatherproof Heavy Parkas |
| ISO 13688:2013 | Ergonomics, Innocuousness & Sizing | REACH Compliant / Zero Harmful Azo Dyes | All Global Commercial Apparel Exports |
As the international textile sector shifts toward environmental accountability and high-tech operational capabilities, procurement directors must align with factories capable of integrating advanced material innovations. Our ongoing product development roadmap highlights four key macro trends dominating winter overcoat manufacturing:
Transitioning from virgin synthetic polyester fills to 100% GRS-certified post-consumer recycled micro-fibers, bio-based Sorona® insulations, and Responsible Down Standard (RDS) verified 700+ fill power down.
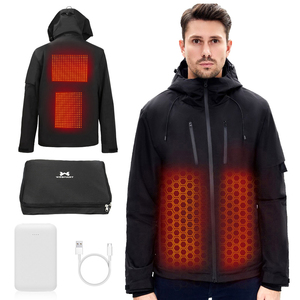
Integration of ultra-thin, flexible graphene heating elements powered by low-voltage USB power packs. Featuring 3-zone independent climate control and auto-shutoff safety sensors.
Adopting non-fluorinated C0 Durable Water Repellent (DWR) surface treatments that meet modern ECHA/REACH regulations without compromising oil and liquid stain barrier properties.
Global apparel brand owners, retail chains, and corporate uniform buyers are restructuring their supply chains to combat geopolitical volatility, fluctuating freight costs, and inventory gluts. Key procurement shifts observed in our global export operations include:
Brands are moving away from traditional import-export agents and trading companies. Direct collaboration with vertically integrated apparel mills provides total visibility over raw yarn selection, fabric weight (GSM) verification, and seam-integrity testing. Removing intermediaries reduces unit costs by 15% to 28% while improving sample iteration velocity.
Rather than ordering 5,000 units per single colorway, modern buyers leverage modular shell platforms. By holding core base fabrics (e.g., 300 GSM heavy wool blend or 75D ripstop nylon) in grey-goods inventory, our factory allows buyers to split bulk orders across multiple styles, colors, and trims with lower Minimum Order Quantities (MOQs starting at 300 pieces per design).
ESG compliance is no longer optional. EU and North American buyers demand verified chain-of-custody documentation for raw materials. Our factory delivers full batch-level traceability—from GOTS (Global Organic Textile Standard) certificates for organic linings to SMETA / HIGG Index social compliance audits covering fair wage distribution and safe working conditions.
Rooted in over 45 years of garment manufacturing expertise, our Ludhiana-based textile complex stands as a premier manufacturing and direct export partner for global brands.
We knit, weave, dye, finish, cut, and stitch under one roof. Our internal laboratory evaluates yarn tensile strength, color fastness (ISO 105-X12), and dimensional stability after washing.
Accelerate your time-to-market using our extensive digital CAD pattern library. Modify existing verified blocks or send your custom tech pack for 100% accurate first-sample prototyping.
Inline visual inspection and final AQL 2.5 / 4.0 audits ensure zero tolerance for structural defects, loose threads, uneven needle tension, or zipper failure prior to container sealing.
