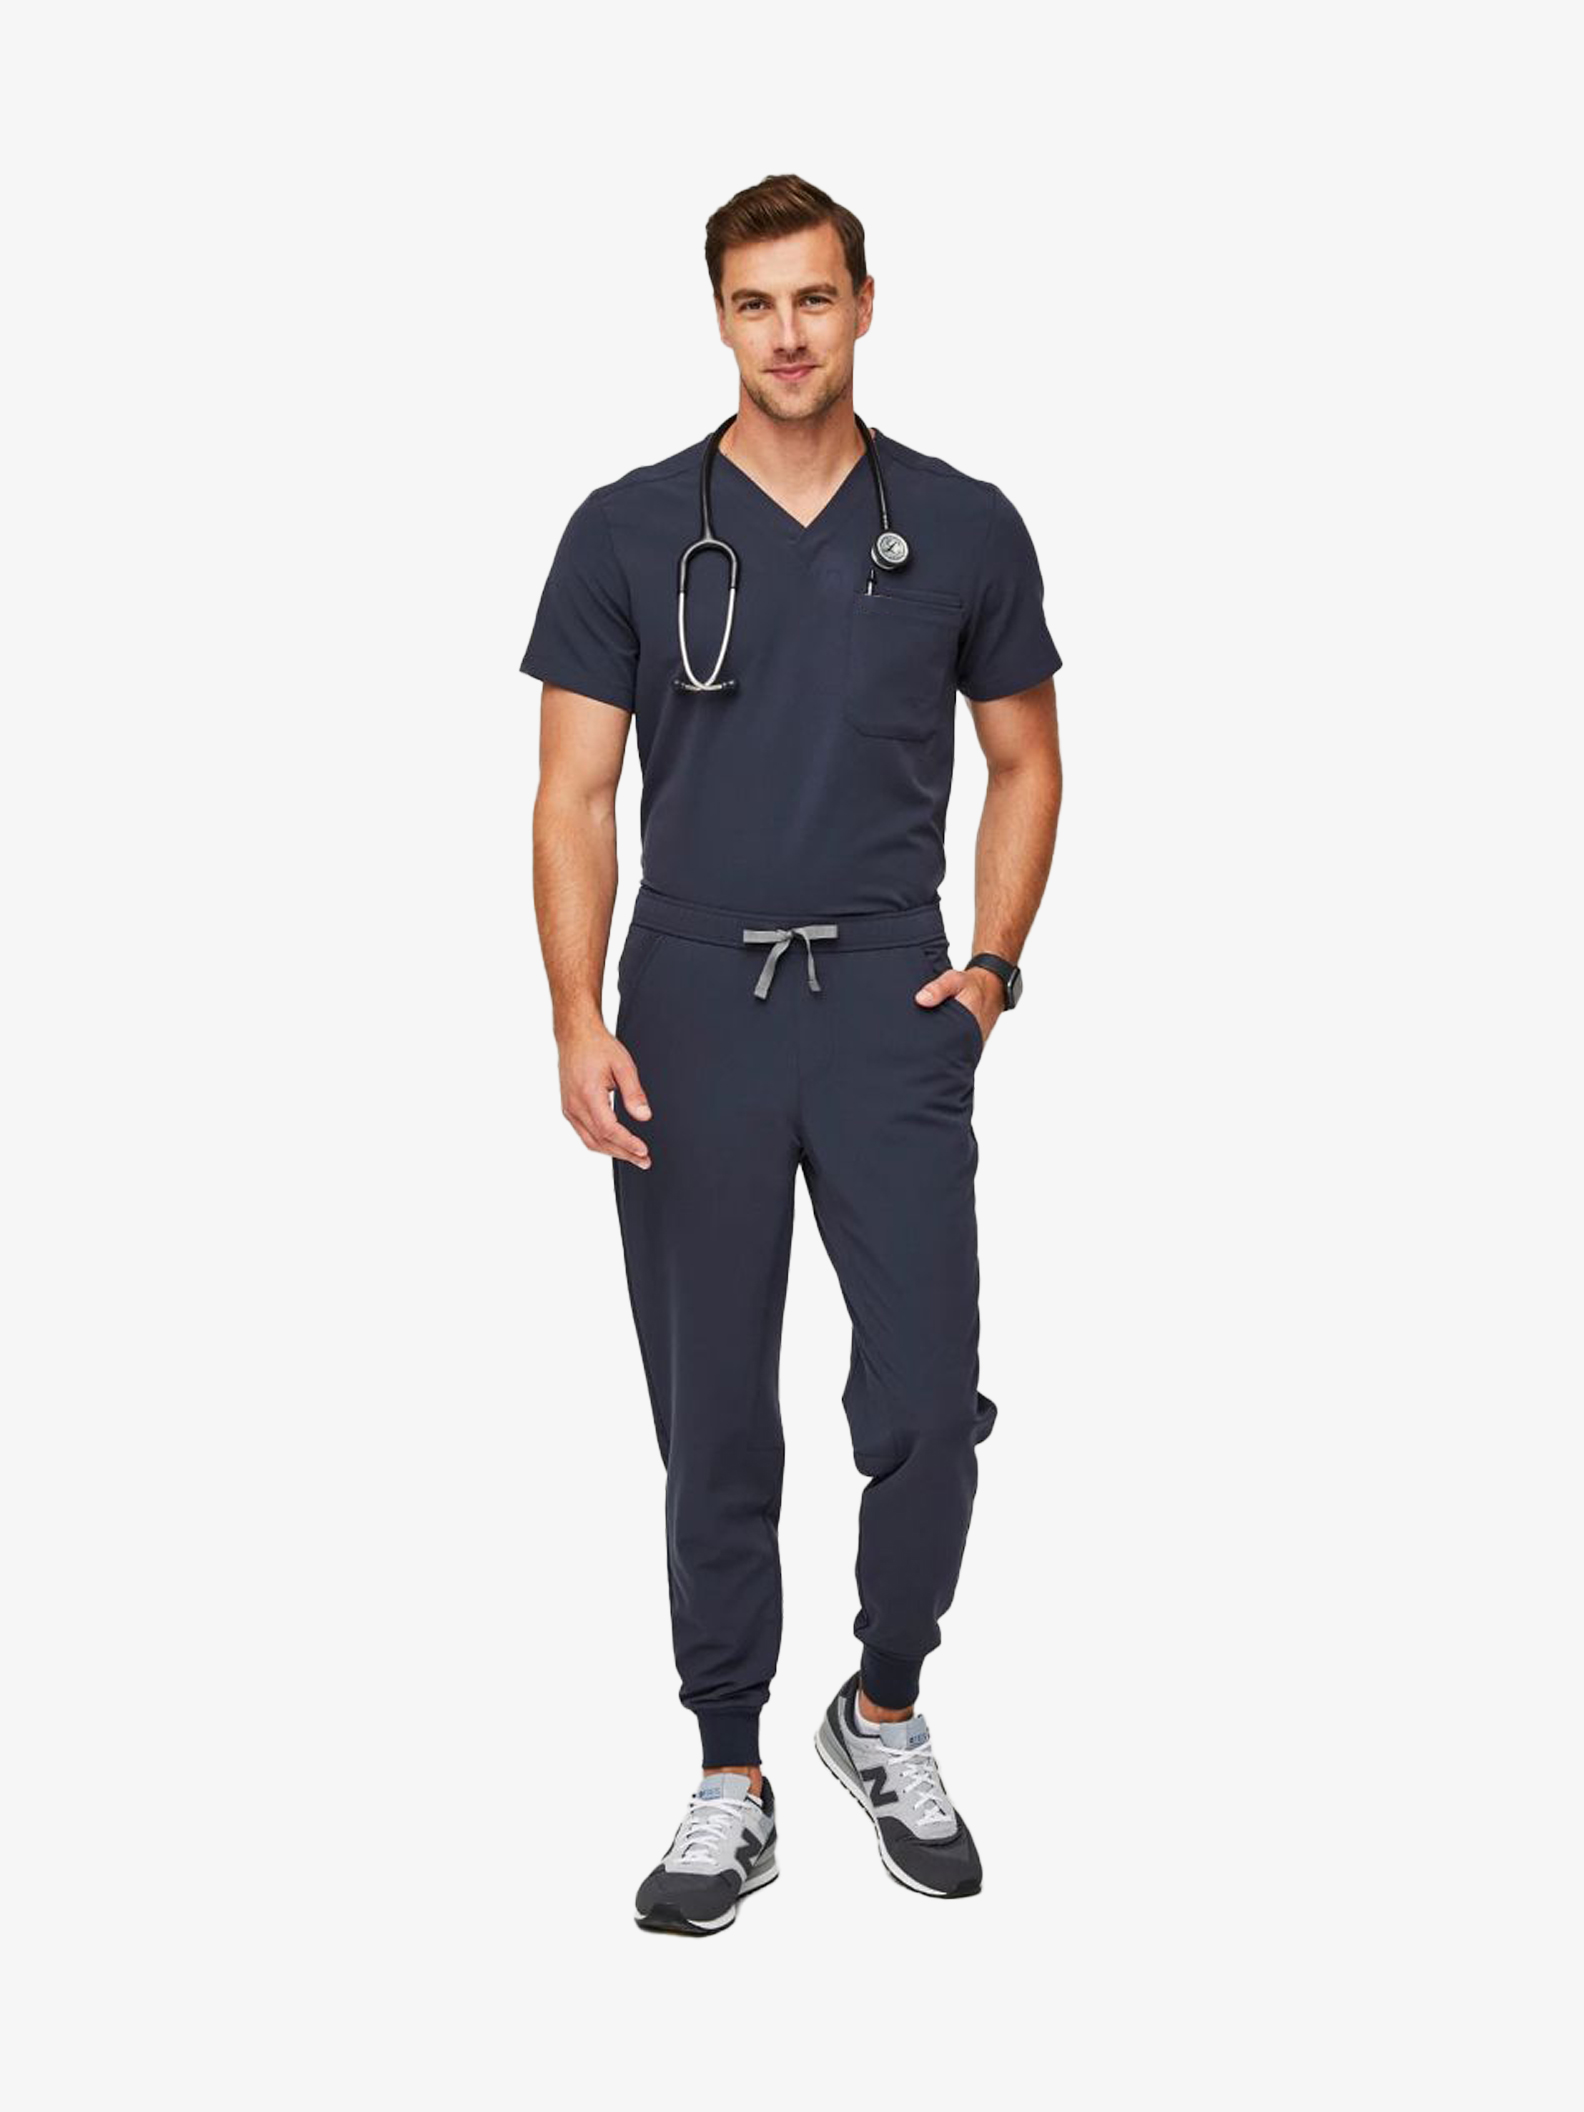
Medical Scrubs & Healthcare Wear
Engineered with silver-ion antimicrobial finishes, fluid resistance, and anti-static properties. Available in multi-pocket designs, mock-wrap tops, and flex-stretch jogger scrubs for healthcare workers.
Vertically Integrated OEM Factory
NG Apparels is a trusted Indian manufacturer and exporter specializing in heavy-duty industrial workwear, medical scrubs, hospitality uniforms, and safety apparel. From 100 GSM lightweight breathable scrubs to 450 GSM flame-retardant industrial coveralls, we engineer custom garments to fit international workplace standards.
Operating directly out of our Ludhiana manufacturing hub since 1981, we handle yarn selection, custom fabric weaving, chemical finishing, CAD block grading, and direct export dispatch without intermediaries. Global brands, healthcare suppliers, and commercial distributors rely on our 45 years of continuous production expertise.

Core Product Line
Every workwear garment is tailored to meet demanding physical environments. We grade patterns across standard XS to 5XL sizing, incorporating reinforced stress points and technical finishes.
Engineered with silver-ion antimicrobial finishes, fluid resistance, and anti-static properties. Available in multi-pocket designs, mock-wrap tops, and flex-stretch jogger scrubs for healthcare workers.
Heavy-duty twill and canvas coveralls designed for manufacturing, mining, and mechanic applications. Built with heavy-duty YKK brass zips, triple-needle lap seams, and tool utility pockets.
EN and ANSI compliant flame-retardant outerwear and shirts. Formulated for oil & gas, welding, and electrical safety with durable FR fabric treatments that withstand standard industrial laundering.
ANSI/ISEA Class 2 and Class 3 reflective vests, jacket shells, and polo shirts. Crafted with certified retroreflective striping and high-chroma fluorescent neon polyester/cotton blends.
Tailored aprons, chef coats, staff polos, and formal button-downs built with stain-release and wrinkle-resistant finishes for luxury hotels, restaurants, and retail enterprises.
Durable ripstop pants, reinforced cargo trousers, weatherproof softshell jackets, and modular tactical vests manufactured with heavy-duty thread and tear-resistant weave structures.
Material & Technical Capabilities
Workwear performance relies heavily on fabric chemistry and structure. Our mill infrastructure processes both natural fibers and advanced synthetic blends, tailored to your required GSM weight and stretch tolerance.
Our technical chemical finishes ensure uniforms maintain protective performance across multiple industrial wash cycles.
Eliminates 99.9% of bacterial buildup, odor, and pathogens on healthcare and food processing uniforms.
Hydrophilic fabric treatments pull sweat away from skin to maintain worker comfort during extreme thermal shifts.
Fluorocarbon-free coatings repel oil, mud, grease, and chemical liquids while maintaining breathability.
Durable press resin finishes prevent creasing during shift work and lower industrial ironing requirements.
Quality Control & OEM Standards
Working directly with our export house removes third-party broker commissions. You communicate straight with technical pattern makers and merchandisers who oversee fabric knitting, garment assembly, and export documentation.
Your tech packs, artwork, pocket structures, and sizing blocks are sealed under non-disclosure conditions. Designs remain your exclusive intellectual property and are never shared with commercial trading agents.
Our workwear undergoes multi-point quality control checks: seam strength tensile testing, color fastness to rubbing and washing, dimensional stability checks, and barcode packaging verifications prior to container loading.
We manage global freight documentation, certificate of origin paperwork, and custom export packing (sealed moisture-resistant master cartons) for smooth door-to-door air express or sea container transport.
Technical FAQ
We offer technical finishes including antimicrobial silver coatings, fluid repellency, flame-retardant finishes compliant with international standards, anti-static treatment, stain release, and high-durability colorfast dyeing designed for industrial laundering.
Our typical MOQ starts at 300 pieces per design, customizable across size sets (XS to 5XL) and colorways. Stock fabric variants can accommodate lower initial trial production volumes.
Yes, we produce flame-resistant coveralls, arc-flash protection garments, and high-visibility reflective safety wear using certified fabrics and retroreflective tape built to EN and ANSI standard guidelines.
All bulk orders undergo strict inline and end-line AQL 2.5 inspection. We test seam tensile strength, colorfastness, shrinkage tolerances, and zipper/trim durability prior to export packaging.
Tech pack evaluation and cost modeling take 3 to 5 business days. Prototype and fit sample development takes 1 to 2 weeks. Bulk manufacturing runs between 4 to 6 weeks depending on quantity and finishing complexity.
Private Label OEM Partner
Send us your technical specification sheet, fabric preference, and quantity breakdown. Our merchandising team will prepare an estimated quote and lead-time analysis within 24 business hours.