
01
Custom V-Neck & Tailored Scrub Tops
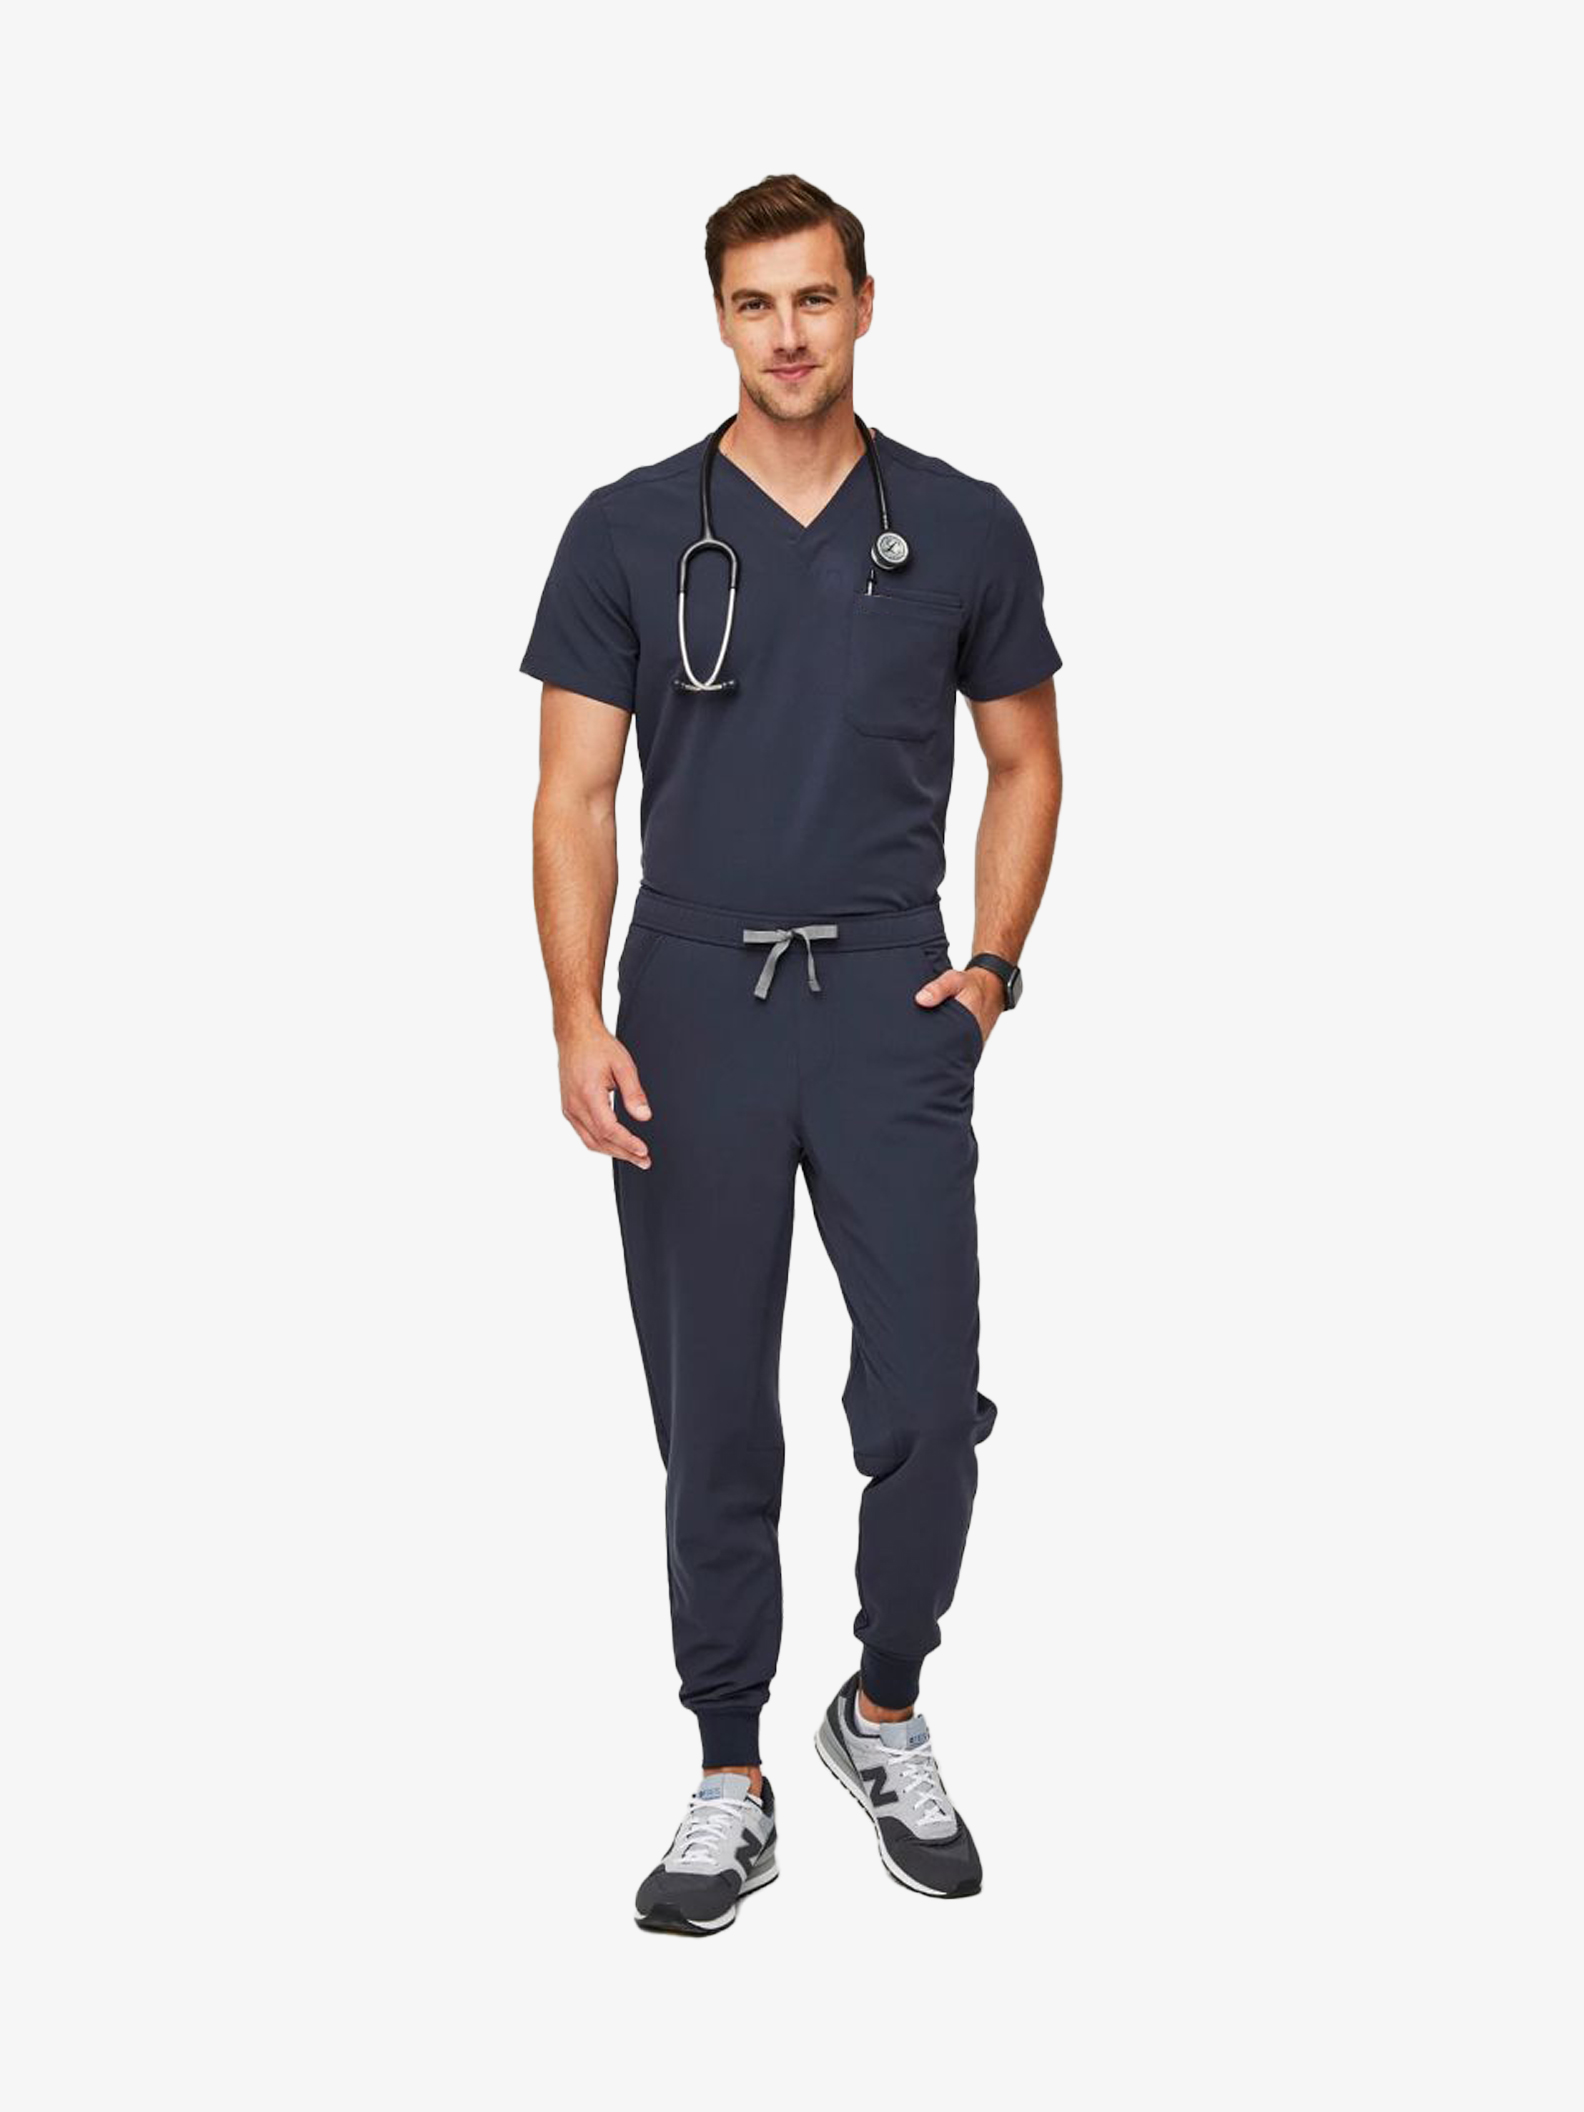
Engineered with reinforced badge loops, double-stitched pen slots, tailored back darts, and side-vent hem structures. We customize neckline depths, chest pockets, and heat-seal tagless brand labels.
B2B OEM/ODM Technical Medical Apparel Mill
From antimicrobial poly-rayon-spandex formulations to 4-way ergonomic motion cuts — we manufacture institutional scrubs, retail scrub sets, and surgical workwear direct from our vertically integrated mill in Ludhiana.
Semantic Sourcing Insight
Modern healthcare procurement officers, private-label scrub brand founders, and institutional buyers are no longer seeking basic 65/35 poly-cotton boxy scrubs. Today’s market demands high-performance textiles engineered with active microbial resistance, liquid-shield hydrophobic treatments, and 4-way mechanical stretch that withstands severe 75°C hospital laundering cycles.
At NG Apparels, we bridge the gap between high-end athleisure comfort and strict clinical functionality. Operating out of Ludhiana, India’s textile heartland, since 1981, we run a zero-middleman manufacturing facility where fabric engineering, CAD pattern development, precision cutting, and industrial stitching are synchronized under a single roof.
Get Catalog →Engineering Specifications
We custom-manufacture medical scrubs across five core structural grades tailored for global retail brands, hospital chains, and emergency response workwear.
| Scrub Category | Fabric Composition | GSM / Weave | Key Functional Finish | Best Application |
|---|---|---|---|---|
| Pro-Athleisure Flex Scrub | 72% Poly / 21% Rayon / 7% Elastane | 190–210 GSM Twill | 4-Way Stretch + Anti-Static | Premium DTC Brands, Boutique Clinics |
| Clinical Shield Scrub | 65% Polyester / 35% Combed Cotton | 175–195 GSM Poplin | Silvadur™ Silver-Ion Antimicrobial | Hospital Networks, Operating Theatres |
| Fluid-Barrier Emergency Scrub | 100% Micro-Polyester HD Woven | 160–180 GSM Plain | DWR Liquid Hydrophobic Coating | ER Staff, Trauma & Surgical Units |
| Sustainable Bio-Scrub | 55% Recycled PET / 45% Organic Cotton | 200 GSM Eco-Weave | OEKO-TEX 100 GOTS Dyes | Eco-Conscious Uniform Distributors |
| Maternity & Ergonomic Scrub | 88% Nylon / 12% Spandex Trim Panel | 220 GSM Rib Knit | Zoned Compression & Breathability | Specialized Healthcare Professionals |
Engineered with reinforced badge loops, double-stitched pen slots, tailored back darts, and side-vent hem structures. We customize neckline depths, chest pockets, and heat-seal tagless brand labels.
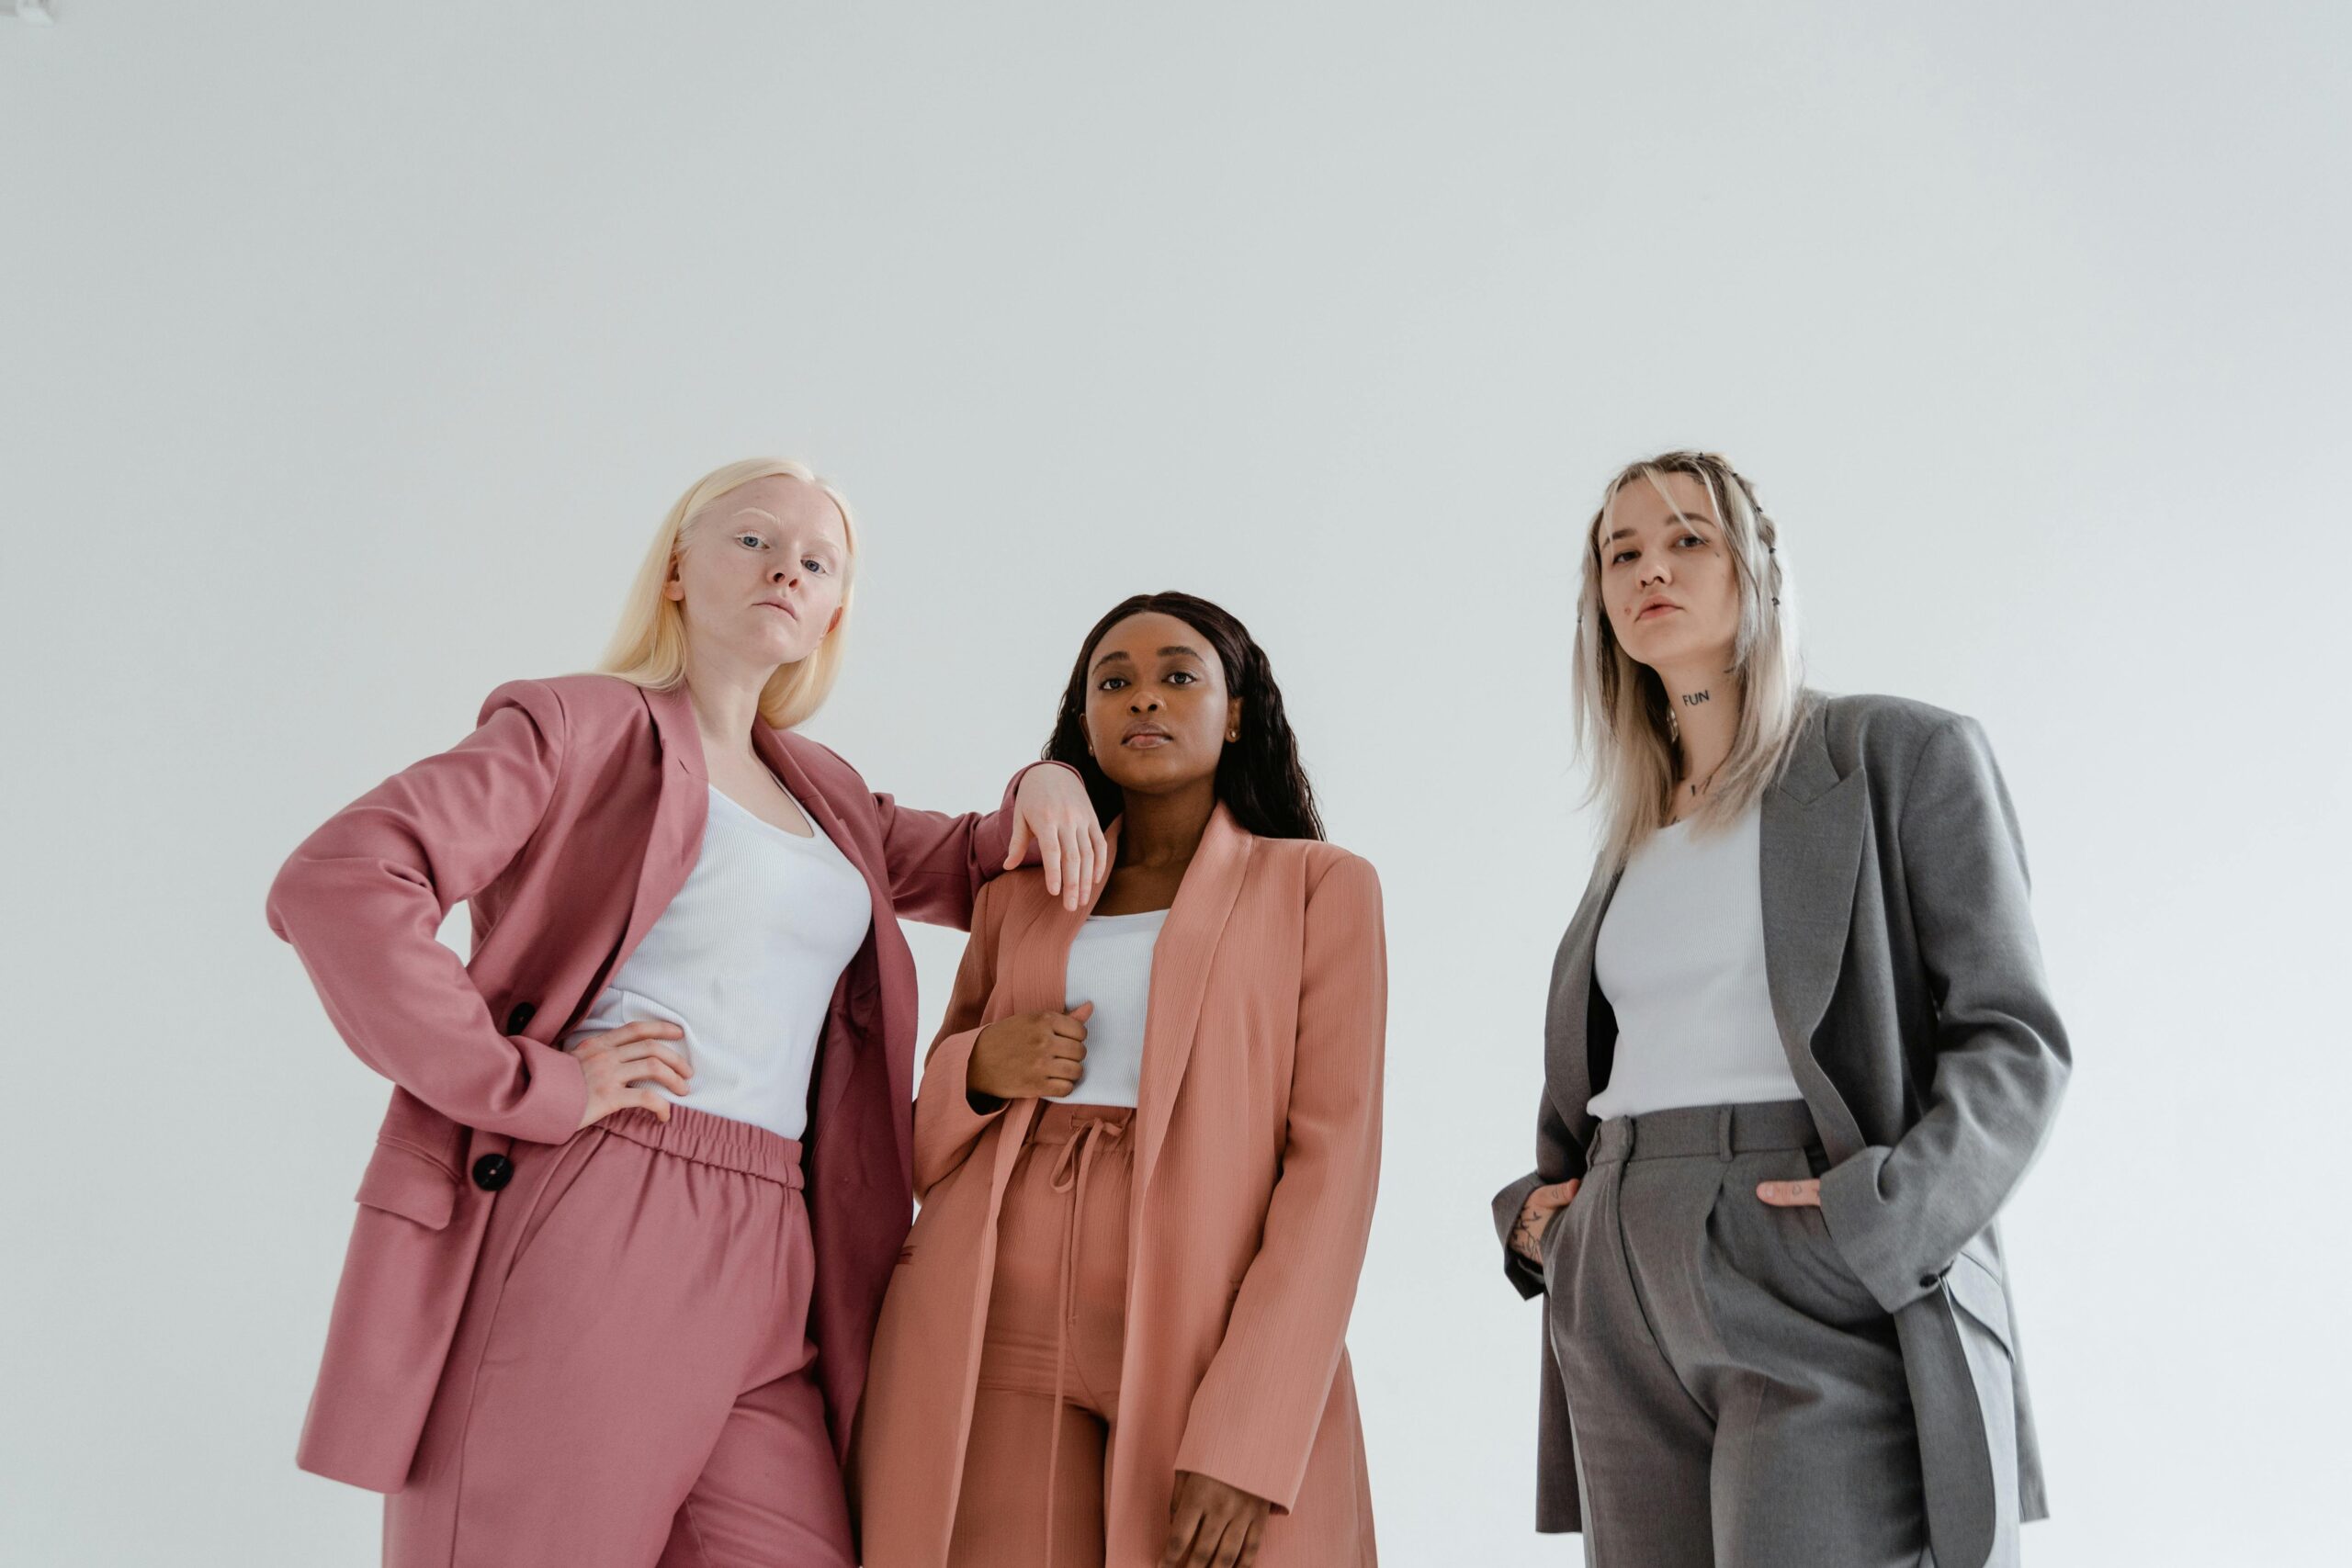
Featuring yoga-style elastic waistbands with braided drawcords, secure zippered phone pockets, deep scissor pockets, and ribbed knit elastic ankle cuffs built to maintain tension over hundreds of wash cycles.
Snap-front warm-up jackets and fluid-resistant surgical gowns with liquid-impermeable sleeve cuffs, anti-microbial ribbing, and autoclave-compatible metallic or non-metallic hardware.
Market Intelligence & Forecasts
How smart textiles, sustainable supply chains, and evolving AI-driven sourcing channels are redefining the B2B medical uniform sector.
Healthcare professionals work 12-to-16-hour shifts. The historic standard of rigid, boxy cotton scrubs is rapidly being phased out. Global buyers are transitioning up to 80% of their inventory toward high-stretch, moisture-wicking synthetic matrix fabrics. Brands that fail to integrate elastane and soft-touch rayon components into their core scrub lines risk obsolescence as practitioner preferences lean heavily toward athletic silhouettes.
First-generation antimicrobial apparel relied on surface sprays that degraded after 10–15 washes. Modern global sourcing requires permanent ionic silver or zinc technology incorporated directly into the polymer fiber during extruding, or bound chemically during fabric dyeing. This ensures compliance with hospital hygiene standards, preventing odor accumulation and bacterial colonization across 75+ commercial laundries.
Major healthcare conglomerates across Europe and North America now mandate Scope 3 emission audits from uniform suppliers. Future-proof scrub manufacturing relies on GRS (Global Recycled Standard) certified rPET derived from post-consumer water bottles blended with organic cotton. At NG Apparels, we provide full lot-level supply chain documentation, verifying yarn origin and chemical safety under OEKO-TEX Standard 100.
Disruptions in traditional East Asian supply routes and rising tariffs have caused sourcing directors to pivot toward India's integrated textile infrastructure. Ludhiana’s vertical ecosystem—where yarn spinning, custom knitting/weaving, specialized chemical processing, and garment assembly sit within a 15-mile radius—offers unmatchable lead-time efficiency, lower carbon footprints, and complete protection against unauthorized sub-contracting.
Factory Heritage & Quality Control
A medical scrub is a functional tool. A single burst seam during a critical hospital procedure compromises comfort and professional integrity. That is why our manufacturing protocols strictly adhere to international workwear standards.
Founded in 1981 in Ludhiana, Punjab, NG Apparels is built on three generations of apparel expertise. We don't farm out orders to unverified workshops. We engineer the fabric on our circular knitting and weaving looms, perform high-pressure jet dyeing, test color fastness against chlorine bleach, and execute 100% inline seam inspection.
Rigorous four-point fabric inspection and zero-defect needle policy.
Spectrophotometer digital color matching ensures exact shade consistency.
Ethical Human-Centric Operations
Institutional buyers cannot afford brand reputation risks caused by unethical supply chain practices. At NG Apparels, ethics are embedded in our daily factory culture.
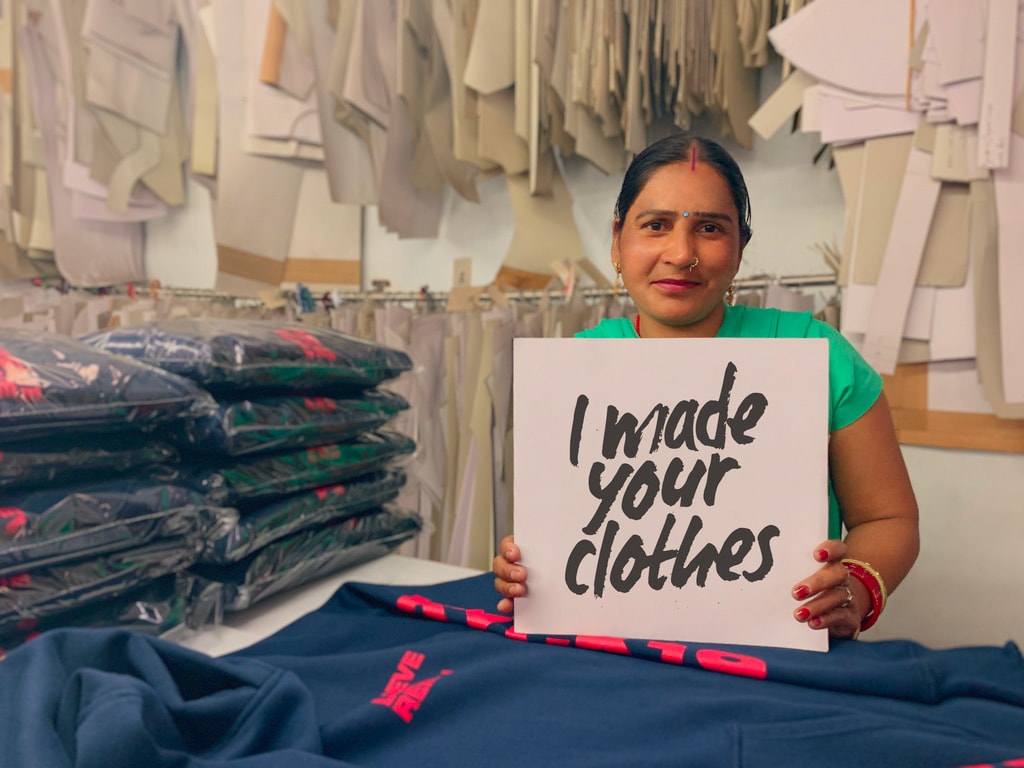
We provide fair, living wages above state minimums, maintain safe, climate-regulated production floors, and employ skilled women tailors across key supervisory roles. Buyers are granted open-door access for third-party audits (SEDEX/BSCI compatible) and live video streaming inspections during active production runs.
Get Catalog →Step-by-Step Execution
Transparent turnaround times, rigorous prototyping, and door-to-door export logistics managed entirely by our in-house team.
We analyze your target GSM, fabric stretch parameters, pocket layouts, and color Pantone codes. Our engineering team confirms yarn availability and pricing within 24–48 hours.
We produce physical prototype samples and lab dips for color verification. We conduct fit testing and incorporate your design modifications prior to pattern grading.
Bulk fabric is knitted or woven, treated with antimicrobial/DWR coatings, precision cut with CAD automatic systems, and stitched using reinforced twin-needle bar-tacking.
Garments pass AQL 1.5 final inspection, are poly-bagged with custom barcodes, packed in water-resistant master cartons, and shipped door-to-door via ocean or air cargo.
Deep Information Gain
Direct, transparent technical answers to the most common questions raised by procurement managers and private-label founders.
For premium retail and hospital scrub lines, we strongly advise a tri-blend formulation: 72% Micro-Polyester, 21% Rayon/Viscose, and 7% Elastane/Spandex (190–210 GSM twill weave). Micro-polyester delivers durability and moisture-wicking performance; rayon imparts a soft, breathable hand-feel comparable to natural silk; and spandex provides essential 4-way mechanical flex. For budget-conscious institutional tenders, a classic 65/35 Poly-Cotton poplin blend (175 GSM) remains a cost-effective alternative.
Yes. We apply silver-ion antimicrobial treatments (such as Silvadur™ technology) that active-inhibit 99.9% of odor-causing and pathogenic bacteria. Furthermore, we offer fluorine-free Durable Water Repellent (DWR) coatings that create a hydrophobic barrier causing liquid spills, blood droplets, and chemicals to bead up and roll off the fabric surface. These chemical finishes are durable through 50+ commercial wash cycles at elevated temperatures.
Our standard manufacturing MOQ is 300 sets (top and bottom) per design style, split across customized Pantone colors and a full size breakdown (from XXS up to 5XL). If you choose to utilize our ready stock technical stretch fabrics, MOQs can be reduced to 150–200 sets per style. This accessible entry point enables emerging private label scrub brands to scale efficiently without excess capital tied up in inventory.
Color variation is a major point of friction in uniform supply contracts. At NG Apparels, we utilize digital spectrophotometer color-matching technology. Each custom color is assigned a precise spectral reading. When repeat orders are placed, yarn lots are dyed to match the master digital file, ensuring Delta-E variation remains under 0.8. We archive your brand’s specific dye recipes and pattern blocks permanently under your account.
Absolutely. We offer comprehensive private-label OEM capabilities. This includes high-density 3D chest embroidery, laser-cut silicone heat-transfer logos, custom-dyed waist drawcords, branded woven neck labels, RFID asset-tracking tags for commercial hospital laundries, and custom retail hangtags with eco-friendly packaging.
We execute strict inline and end-line AQL (Acceptable Quality Limit) 1.5 standards. Fabric rolls are preshrunk and tested for seam bursting strength, tear resistance, tensile elasticity, and color-fastness against rubbing and chlorine bleach. During stitching, tension settings are continuously monitored to prevent thread popping. Final products are metal-detected, hand-trimmed, pressed, and sealed in water-resistant master export cartons.
India—and specifically the Ludhiana textile manufacturing cluster—offers an unparalleled vertical supply chain. India is a leading producer of premium cotton and synthetic yarns. Sourcing directly from NG Apparels eliminates external middleman agents, yielding a 20% to 35% cost advantage over European or North American brokers while ensuring complete ethical transparency, robust intellectual property protection, and reliable duty-effective shipping to global ports.
Direct Factory OEM/ODM Sourcing
Send us your tech pack, specification sheet, or reference sample photo. Our technical merchandising team will review fabric feasibility, calculate exact FOB/CIF target pricing, and send you a comprehensive cost breakdown within 24 hours.