NG Apparels — clothing manufacturer India logo
Our Story +
Products +
Ethical Manufacturing
Resource +
FAQs Contact Us

OEM/ODM Thermal Underwear Manufacturer & Exporter

Precision Fiber Engineering · Seamless Circular Knitting · Global B2B Supply Solutions

Turnkey Thermal Underwear Solutions for Private Labels

Custom-engineered thermal base layers crafted with advanced moisture management, seamless body-mapping technology, and sustainable certified yarns.
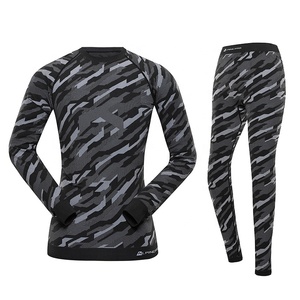
Alpine PRO Men's Breathable Ski Underwear Set Winter Sports Thermal Underwear
Alpine PRO Men's Breathable Ski Thermal Underwear Set
  • Fabric: 260 GSM Polyester-Spandex Micro-Fleece
  • Tech: Ergonomic Compression & Quick-Dry
  • Application: Sub-Zero Winter Sports & Outdoor Skiing
Contact Us
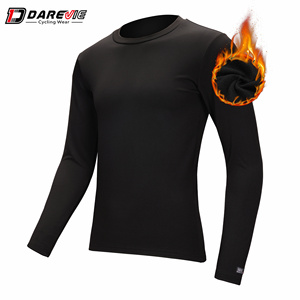
Underwear Shirts Cycling Base Layer Men Thermal Underwear Custom Men's Thermal Long Sleeve
Performance Cycling Base Layer Long-Sleeve Thermal Top
  • Fabric: 210 GSM Hydrophobic Polypropylene Blend
  • Tech: Dynamic Sweat Wicking & Anti-Chafing Flatlock
  • Application: Endurance Cycling, Running & Athletics
Contact Us
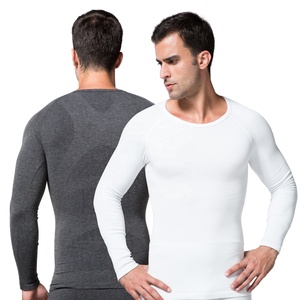
W067 Thermal Underwear Seamless HEATMAX Compression Thermo Top Slimming Plus Size
HEATMAX Seamless Compression Slimming Thermo Top
  • Fabric: Seamless Santoni 3D Knit Nylon-Elastane
  • Tech: Targeted Thermal Density & Body Shaping
  • Application: Plus-Size Comfort & Daily Insulation
Contact Us
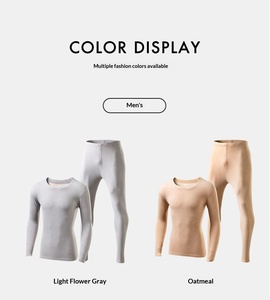
Unisex Cotton Wool Silk Thick Thermal Underwear Set Warm Breathable Waterproof
Luxury Tri-Blend Cotton Wool Silk Thick Thermal Set
  • Fabric: 320 GSM Merino Wool, Natural Silk & Organic Cotton
  • Tech: Natural Thermoregulation & DWR Water Repellency
  • Application: Extreme Cold Weather & Luxury Activewear
Contact Us
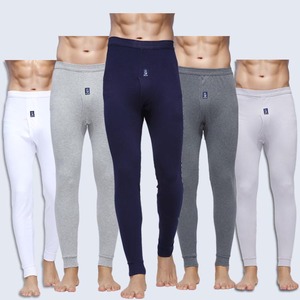
Men's Eco-Friendly Cotton Thermal Underwear Pant Breathable All-Seasons Machine-Washable
Men's Eco-Friendly Organic Cotton Thermal Long Johns
  • Fabric: 240 GSM GOTS Certified Organic Cotton Rib
  • Tech: Anti-Shrinkage Treatment & Machine-Washable
  • Application: All-Season Sustainable Loungewear
Contact Us
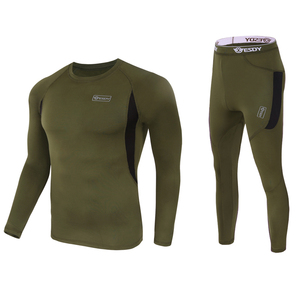
ESDY Outdoor Sports Warm Fleece Underwear Set Long Johns Tactical Thermal Cycling Clothing
Tactical Grade Grid-Fleece Heavyweight Thermal Set
  • Fabric: 280 GSM Honeycomb Grid Fleece
  • Tech: High Warmth-to-Weight Ratio & Vapor Channels
  • Application: Tactical, Hunting, Hiking & Heavy-Duty Outdoor
Contact Us
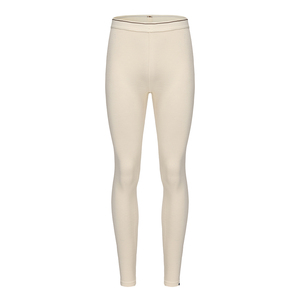
Women's Merino Wool Eco-Friendly Outdoor Long Johns Breathable Anti-Bacterial Thermal Underwear Legging
Women's Ultra-Fine Merino Wool Seamless Base Layer
  • Fabric: 100% Australian Merino Wool (18.5 Micron)
  • Tech: Natural Odor Resistance & Antibacterial Shield
  • Application: Alpine Trekking & Premium Winter Retail
Contact Us
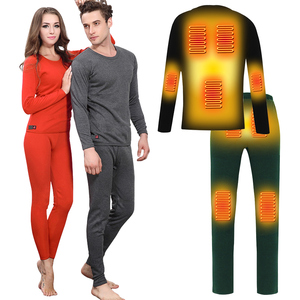
Adult Heated Underwear Set Winter Snow Outdoor Sports Home Thermal Clothing With Heated Baselayer
Smart Carbon-Fiber Heated Thermal Baselayer Set
  • Fabric: Spandex-Polyester Composite with Micro-Heaters
  • Tech: 3-Zone App Controlled Temperature Heating
  • Application: Extreme Sub-Zero Operations & Snow Sports
Contact Us
45+
Years Manufacturing Heritage
2,400+
Global Brands Served
3,000+
In-House Pattern Libraries
7-9 Wks
Tech Pack to Door Delivery

Engineering Superiority in Custom Thermal Garment Manufacturing

Founded in 1981, our state-of-the-art facility in Ludhiana, India, has established itself as an authoritative global manufacturing hub for high-performance functional base layers, seamless compression garments, and technical thermal underwear. Spanning over four decades of textile mastery, we operate under a completely vertically integrated model—controlling every micro-stage from raw yarn selection, circular knitting, and eco-friendly piece dyeing to computer-aided pattern grading, flatlock stitching, and direct export logistics.

Direct-from-Factory Accountability: By completely removing intermediary sourcing agents and purchasing brokers, we ensure your confidential tech packs stay protected inside our facility while delivering a 15–22% cost efficiency direct to your margin.
01

In-House Fabric Engineering

We do not rely on standard market stock fabrics. Our mills custom-knit single jersey, ribbing, double-face interlock, and grid fleece ranging from 140 GSM to 400 GSM, tailored specifically to your target GSM, elasticity, shrinkage tolerance, and tactile hand-feel.

02

Advanced Seamless Circular Knitting

Utilizing high-gauge Santoni seamless knitting machines, we engineer zonal compression garments with anatomically mapped ventilation zones, muscle-support structures, and zero-seam comfort to prevent abrasion during high-output activity.

03

Rigorous AQL Quality Control

Every order undergoes strict Inline and End-line inspections executing AQL 1.5/2.5 standards. Fabric batches undergo rigorous colorfastness testing, burst strength analysis, shrinkage testing, and nickel-release verification for all hardware.

📊 Industry Whitepaper: Thermal Underwear Fabric Matrix

Understanding the material science behind modern base-layer thermal efficiency (CLO values), moisture transport, and antibacterial resilience.

Fabric Composition GSM Range CLO Value (Insulation) Moisture Wicking Rate Key ODM Customization Features
100% Ultrafine Merino Wool 180 - 260 GSM 0.35 - 0.48 / oz High (Vapor Absorption) Lanolin-retained natural antibacterial finish, anti-felting treatment, flatlock ISO 607 stitching.
Polypropylene & Nylon Blend 160 - 220 GSM 0.28 - 0.38 / oz Exceptional (Hydrophobic) Zero water retention, super-lightweight density (0.91 g/cm³), seamless body-mapped construction.
Honeycomb Grid Fleece (Tactical) 250 - 340 GSM 0.45 - 0.62 / oz Moderate to High Brushed inner air-trapping channels, DWR outer shell coating, reinforced elbow & knee patches.
GOTS Organic Cotton-Spandex Rib 200 - 280 GSM 0.22 - 0.32 / oz Moderate 100% traceable organic supply chain, bio-wash soft finish, hypoallergenic skin contacts.
PCM (Phase Change Material) Synthetics 220 - 290 GSM Dynamic Adjusting High (Active Evaporation) Micro-encapsulated thermoregulation paraffin waxes absorbing heat during exertion & releasing when cold.

Key Technical Trends Reshaping Thermal Base Layer Manufacturing

The global thermal underwear market has transitioned from passive cold-weather insulation to active micro-climate management. Consumer demand is driven by technical performance, body-mapped ergonomics, eco-sustainability, and integrated active heating technologies. As an industry-leading OEM/ODM manufacturer, we implement the following next-generation manufacturing processes:

1. Biomimetic Push-Pull Moisture Management

Modern functional base layers utilize dual-layer bi-component knitting architectures. The inner layer consists of hydrophobic fibers (such as polypropylene) that draw liquid sweat away from the skin instantly, while the outer hydrophilic layer (such as micro-polyester or wool) spreads sweat across a large surface area for rapid evaporative cooling during high activity.

2. Active Carbon & Graphene Infused Fibers

By spinning graphene micro-particles or conductive carbon filaments directly into the synthetic polymer matrix, we manufacture thermal underwear that exhibits far-infrared (FIR) heat reflectivity, natural antistatic properties, and permanent antimicrobial efficacy that never washes out over 50+ industrial laundering cycles.

3. Eco-Friendly Circularity & GOTS/GRS Compliance

With tightening environmental regulations, private labels are rapidly shifting toward Global Recycled Standard (GRS) certified recycled polyamides (ocean plastic waste) and GOTS-certified organic cotton. Our dye houses utilize low-liquor-ratio machines reducing water consumption by 40% and utilizing OEKO-TEX Standard 100 Class I non-toxic dyes.

4. Micro-Tronics & Smart Heated Apparel Integration

OEM heated base layers represent the fastest-growing segment in extreme-cold sport apparel. We engineer specialized garment channels designed to house flexible carbon-fiber heating pads and low-profile battery connectors, combining waterproof sealing technology with washable circuit loops.

5. 3D Body-Mapping & Variable Compression

Using CAD-driven Santoni knitting software, we design thermal tops and leggings with multi-density zonal knitting. High-sweat zones (spine, underarms) feature breathable mesh perforations, while core muscle groups receive targeted compression support to improve blood circulation during ski runs or tactical exercises.

6. Mechanical & Chemical Specialty Finishes

We provide proprietary surface treatments including Durable Water Repellent (DWR) C0 non-fluorinated coatings, silver-ion antibacterial shields, aloe-vera skin conditioning washes, and anti-pilling enzymatic treatments for cotton and fleece thermal fabrics.

Future Procurement Trends for Thermal Apparel Buyers (2025–2030)

Navigating international apparel procurement requires balancing cost competitiveness, lead-time flexibility, regulatory transparency, and uncompromised product quality. Based on global retail sourcing data, apparel buyers should structure their supply chain strategy around three key pillars:

1. Shift Toward Vertically Integrated Asian Hubs: Brands are increasingly consolidating vendor rosters to factories that own both fabric mills and cut-and-sew operations. This eliminates raw material transport delays, reduces fabric lead times by 14 days, and ensures unified color shade matching across matching sets.
2. EU Digital Product Passport (DPP) & Traceability Preparedness: Global buyers exporting to Europe and North America must ensure full supply chain traceability from raw yarn origin to final garment assembly. Our facility provides certified lot-level documentation for organic cotton, recycled synthetics, and mulesing-free wool.
3. Agile Production Runs & Low MOQ Prototyping: To mitigate inventory holding risks caused by unpredictable winter weather cycles, procurement teams are favoring flexible OEM factories capable of executing modest initial orders (300 pcs/style) with rapid bulk scale-up capacity within 4 to 6 weeks.

Frequently Asked Questions (OEM/ODM Thermal Underwear)

Q1: What is your Minimum Order Quantity (MOQ) for custom OEM/ODM thermal underwear?
Our standard Minimum Order Quantity (MOQ) is 300 pieces per style, which can be split across standard colorways and size breakdowns (S through 3XL). For styles utilizing in-stock, factory-supported technical fabrics (such as standard combed cotton rib or micro-polyester fleece), we can accommodate lower launch quantities. Custom yarn-dyed or specialized knitted fabrics require higher minimum volumes due to dye-house vat capacities.
Q2: How long is the timeline from initial tech pack submission to bulk delivery?
The typical production cycle spans 7 to 9 weeks:
Week 1: Tech pack evaluation, yarn availability check, and formal costing confirmation.
Weeks 2–3: Prototype development, lab-dip color approval, and pre-production (PP) fit sample approval.
Weeks 4–8: Bulk fabric knitting, dyeing, cutting, flatlock assembly, and AQL 1.5/2.5 inspection.
Week 9: Export packing and dispatch via door-to-door air freight (5–8 days) or sea freight (4–6 weeks).
Q3: Do you offer fully custom branding, private label trims, and retail packaging?
Yes, we provide end-to-end private label customization. This includes custom heat-transfer back-neck labels, high-density woven brand tags, silicone care labels, custom branded waistbands, custom hangtags with barcoding, and eco-friendly biodegradable frosted polybags or printed retail boxes.
Q4: How do you verify and guarantee thermal insulation ratings (CLO values)?
Our in-house textile laboratory tests fabric samples for Thermal Resistance (RCT) according to ISO 11092 and ASTM F1868 standards. We measure air permeability (mm/s) and Moisture Vapor Transmission Rate (MVTR) to ensure optimal warmth-to-weight performance before bulk production commences.
Q5: Can you manufacture eco-friendly and certified sustainable thermal clothing?
Absolutly. We regularly manufacture thermal sets using GOTS-certified organic cotton, GRS-certified recycled polyester (rePET), recycled polyamide, bamboo viscose, and non-mulesed ethically sourced Australian Merino wool. Full material certificates of compliance are provided with every export shipment.
Q6: How are design intellectual property and tech packs protected?
Because we manufacture 100% in-house within our owned facilities in Ludhiana, your tech packs and proprietary pattern blocks are never distributed to third-party sub-contractors or buying agencies. We sign binding Non-Disclosure Agreements (NDAs) prior to sample development to guarantee complete brand confidentiality.

Ready to Manufacture Your Custom Thermal Line?

Partner with an authoritative, family-owned Indian apparel manufacturer with 45+ years of export expertise. Send us your design specifications or tech packs for instant costing and sample scheduling.

Contact Us