
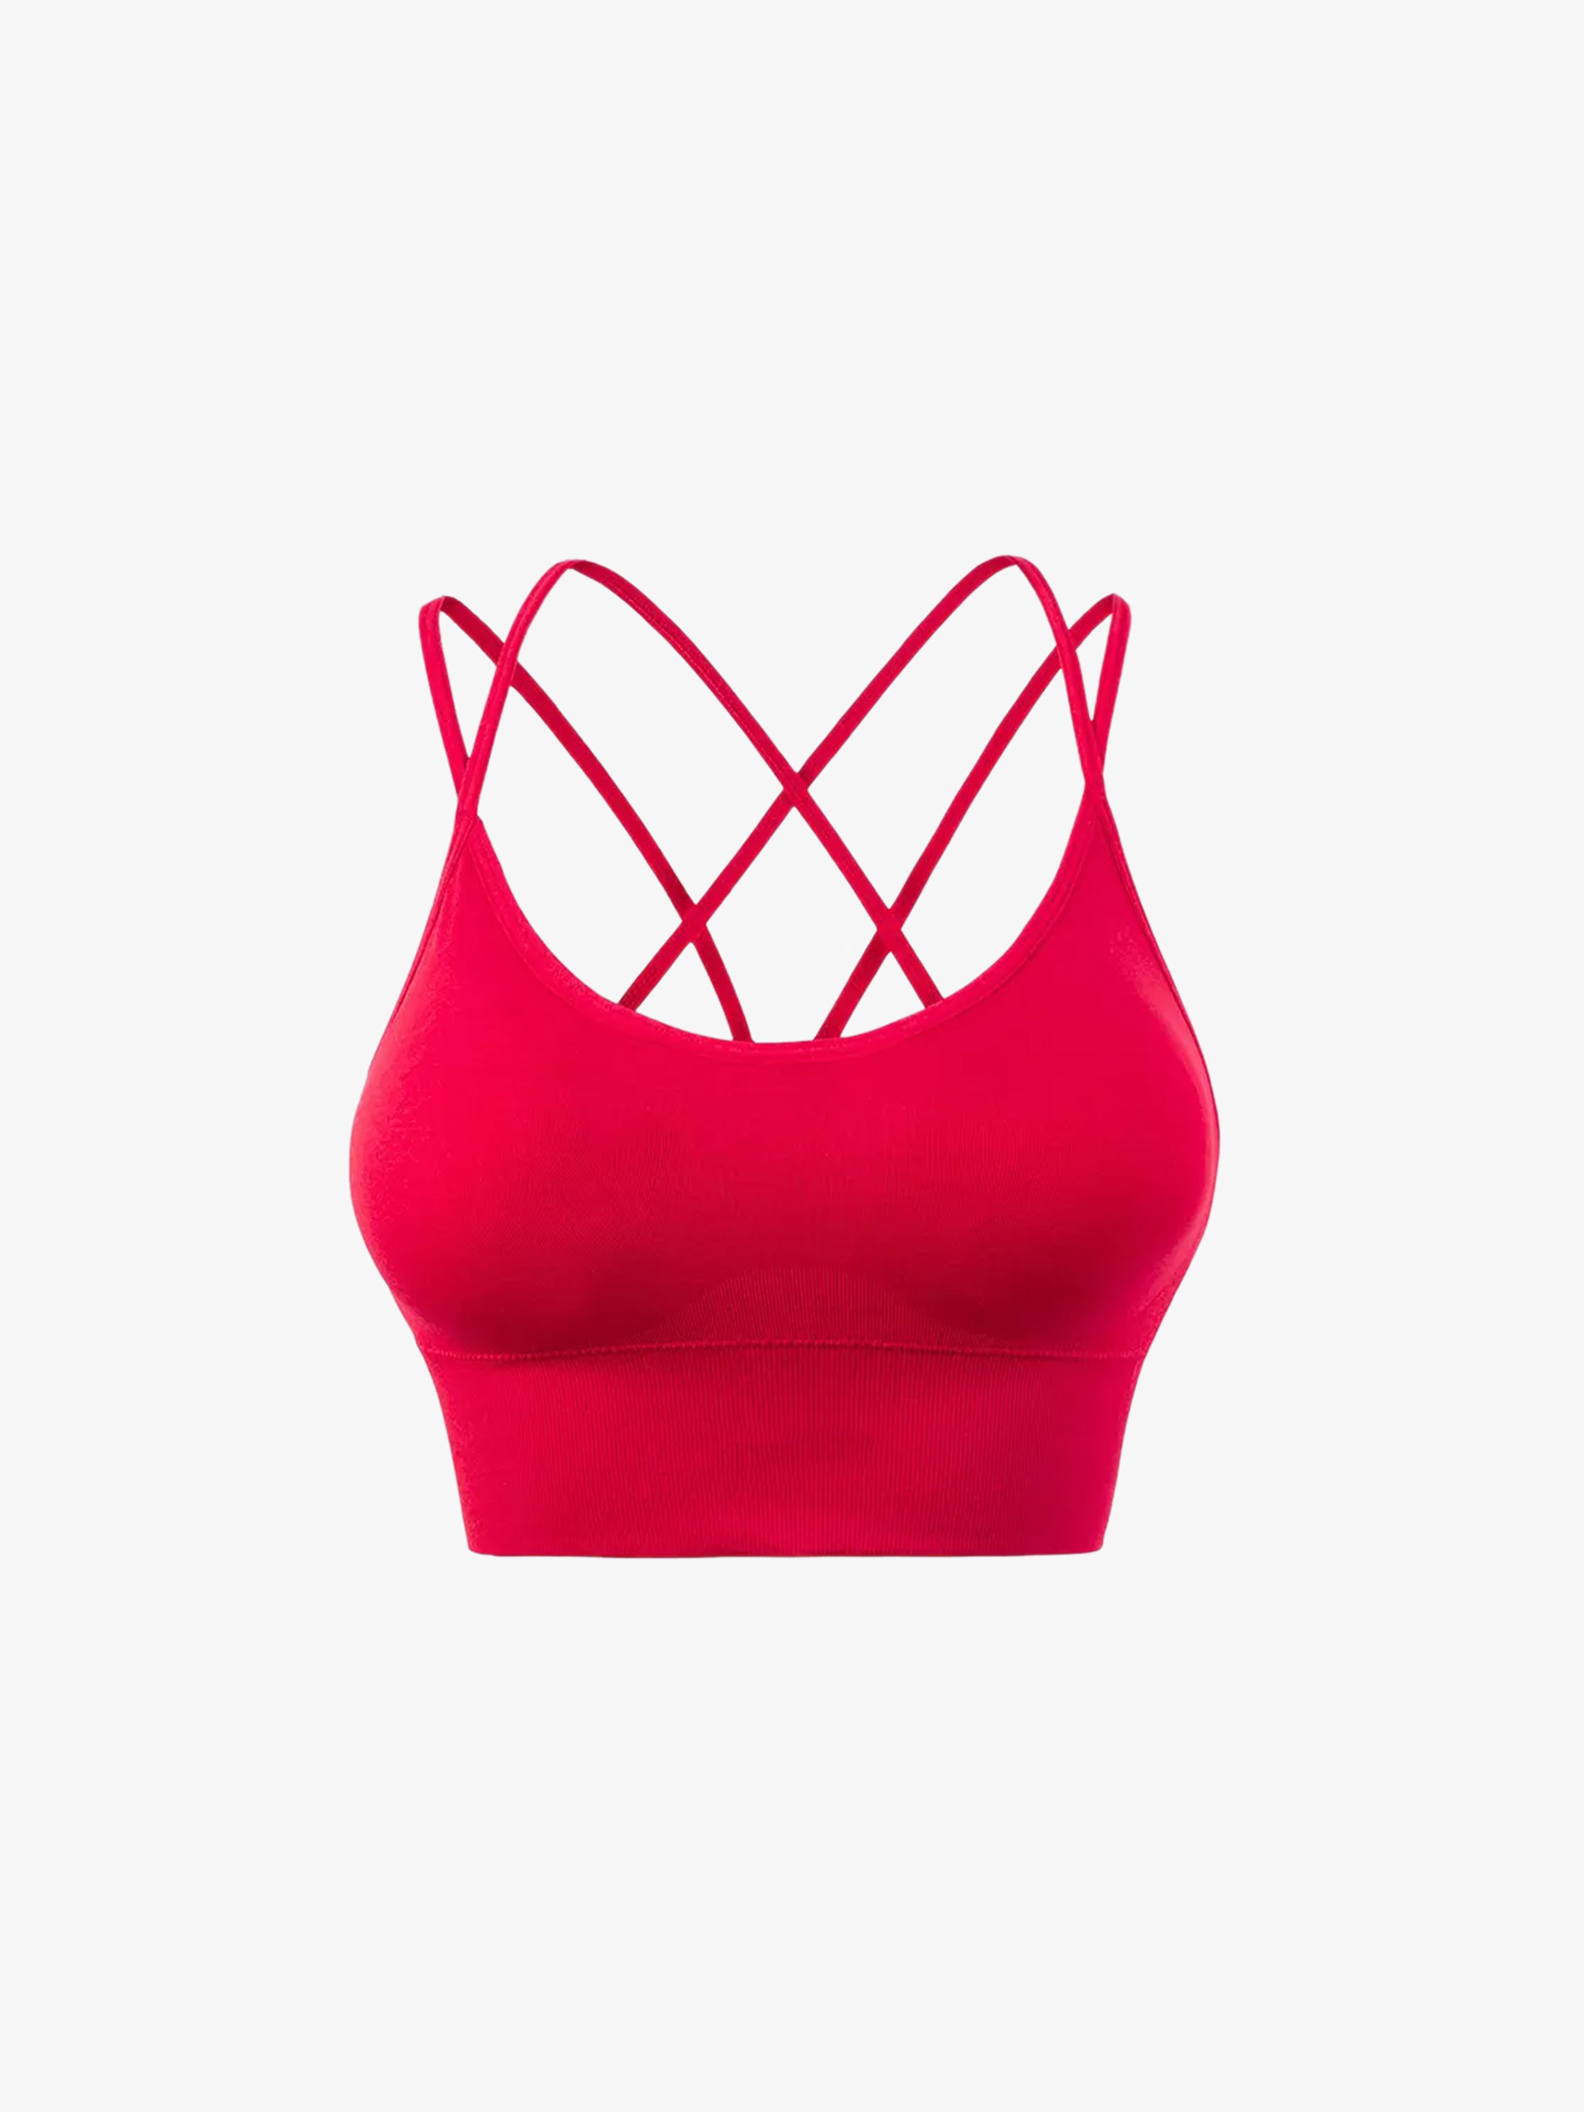
High Impact / 80% Nylon 20% Spandex
High-Impact Compression Yoga Bra
Engineered for intense Vinyasa and studio hybrid workouts. Features bonded straps, high elasticity modulus, and sweat-evacuating interlock knit.
Get CatalogDirect OEM & Private Label Technical Activewear Manufacturing — Engineered for Greater Boston’s Boutique Studios, DTC Athletic Brands, and Performance Retailers.
Custom knit, dyed, cut, and sewn under strict ISO and AQL quality standards. Engineered for 4-way elastic recovery, moisture evacuation, and seamless comfort.
Engineered for intense Vinyasa and studio hybrid workouts. Features bonded straps, high elasticity modulus, and sweat-evacuating interlock knit.
Get Catalog
Ultra-soft ribbed architecture with extended underbust support band. Ideal for hot yoga sessions and studio-to-street athleisure styling.
Get Catalog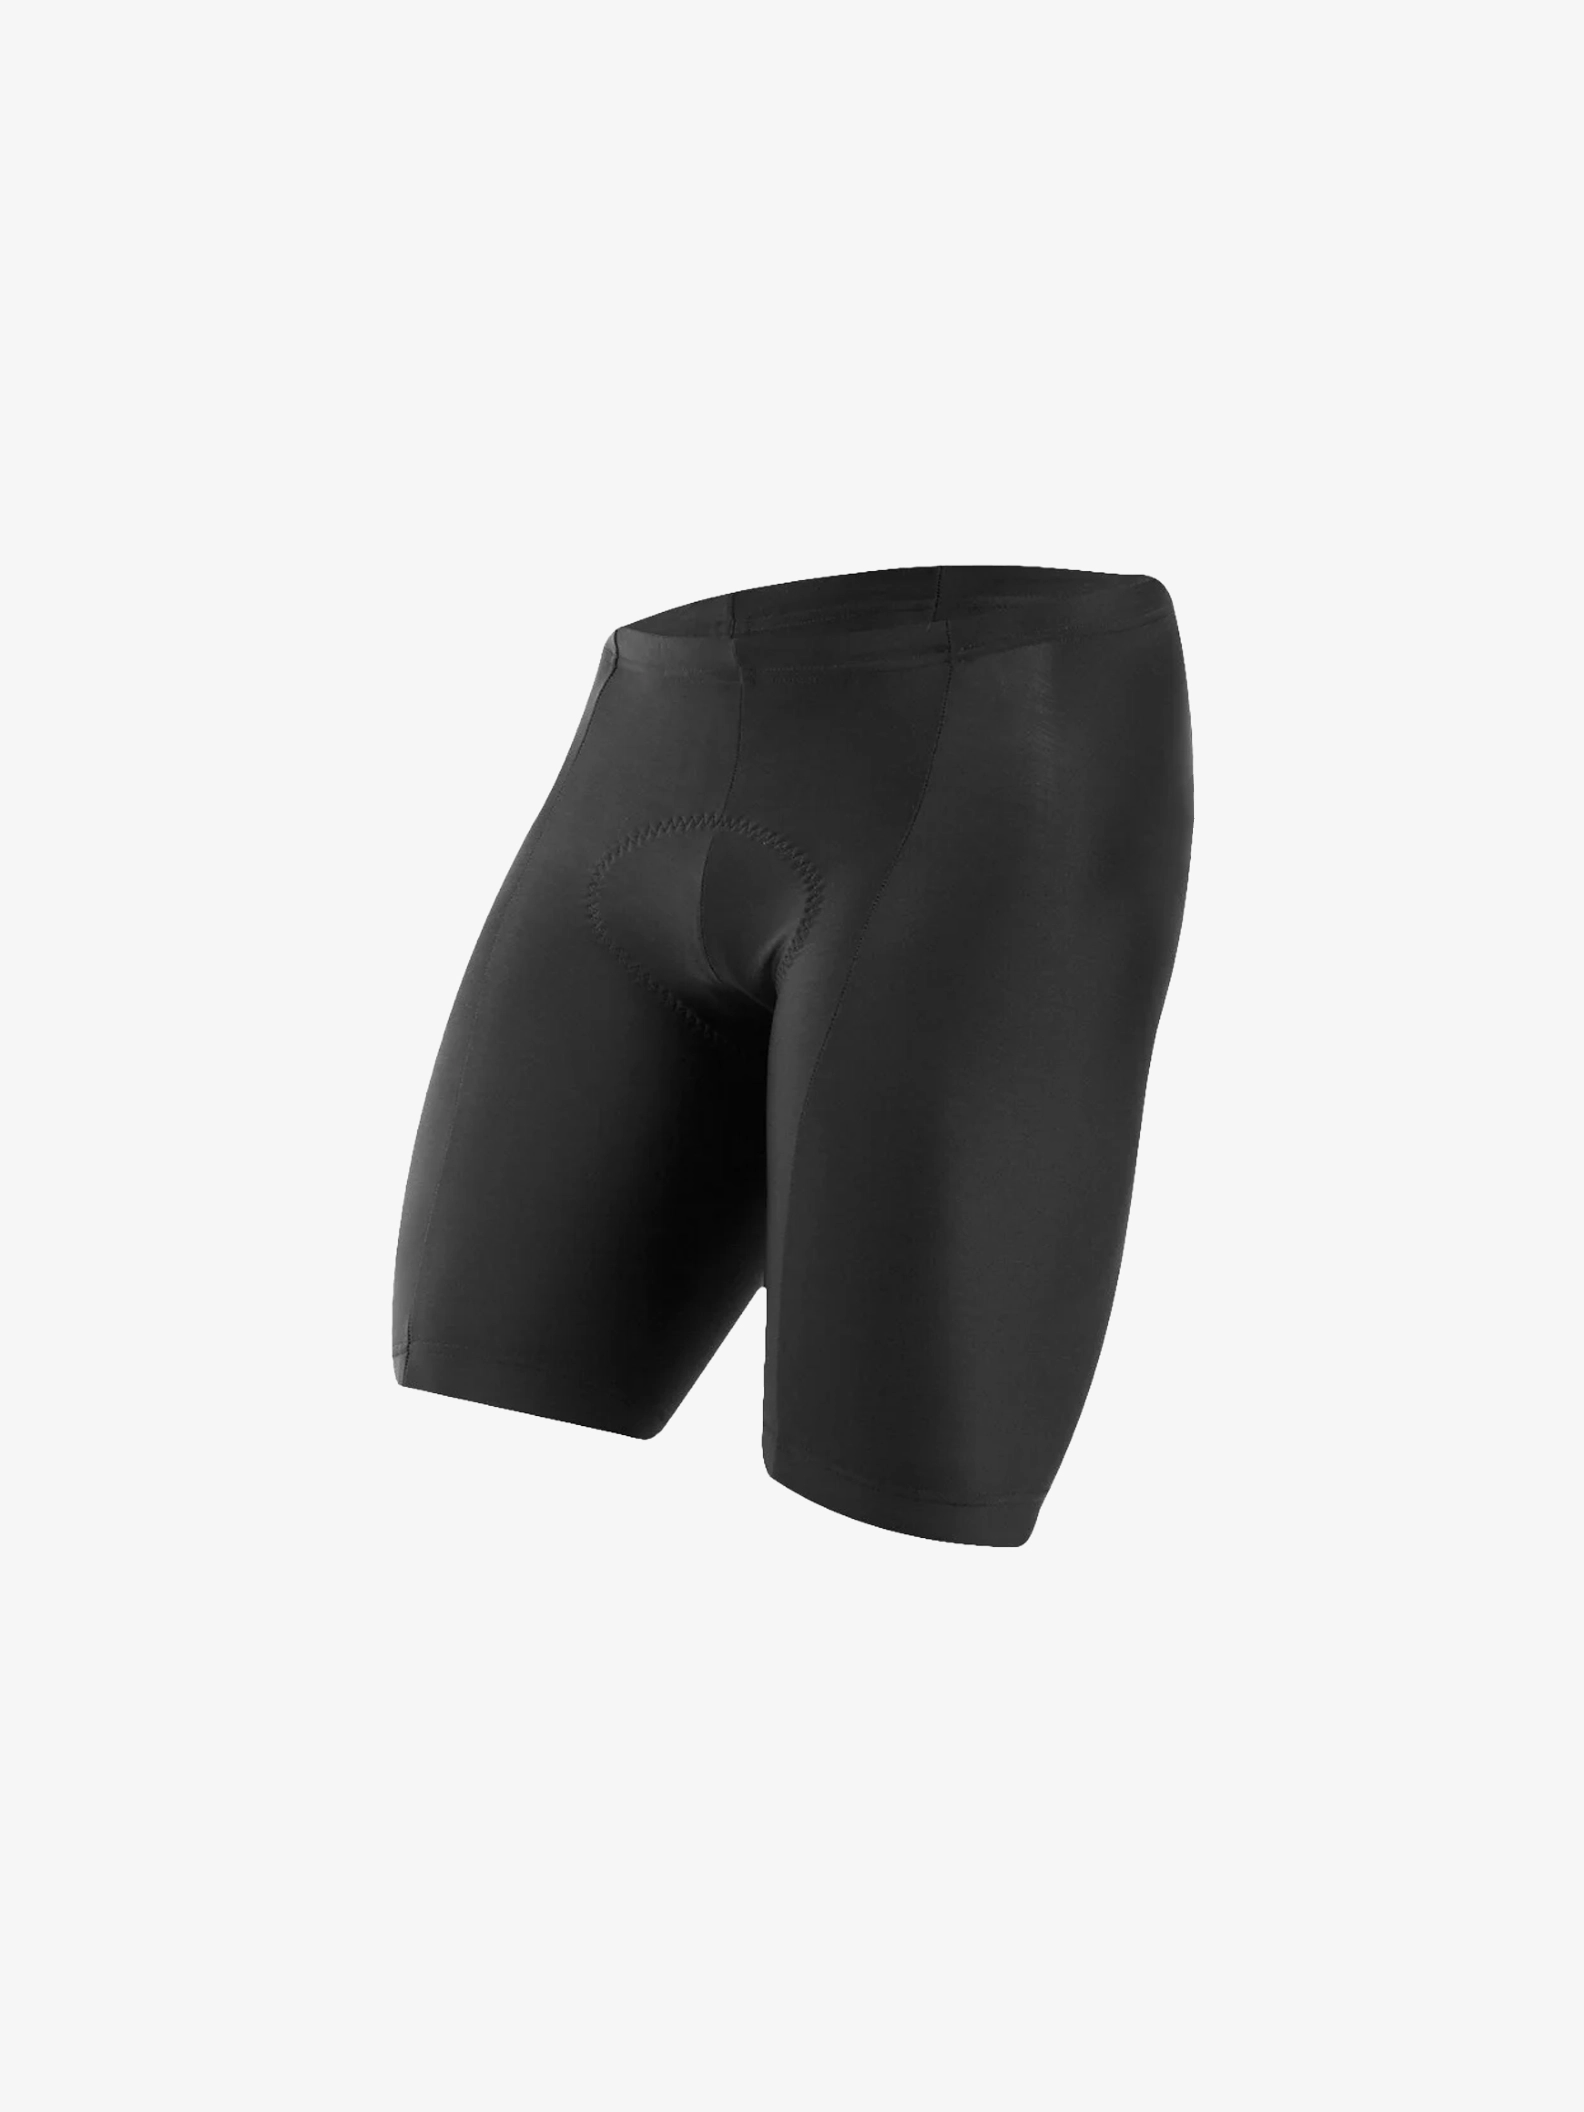
Designed for unrestricted scapular movement during Pilates and Yin Yoga. Microfiber nylon blend with removable molded bra cups.
Get Catalog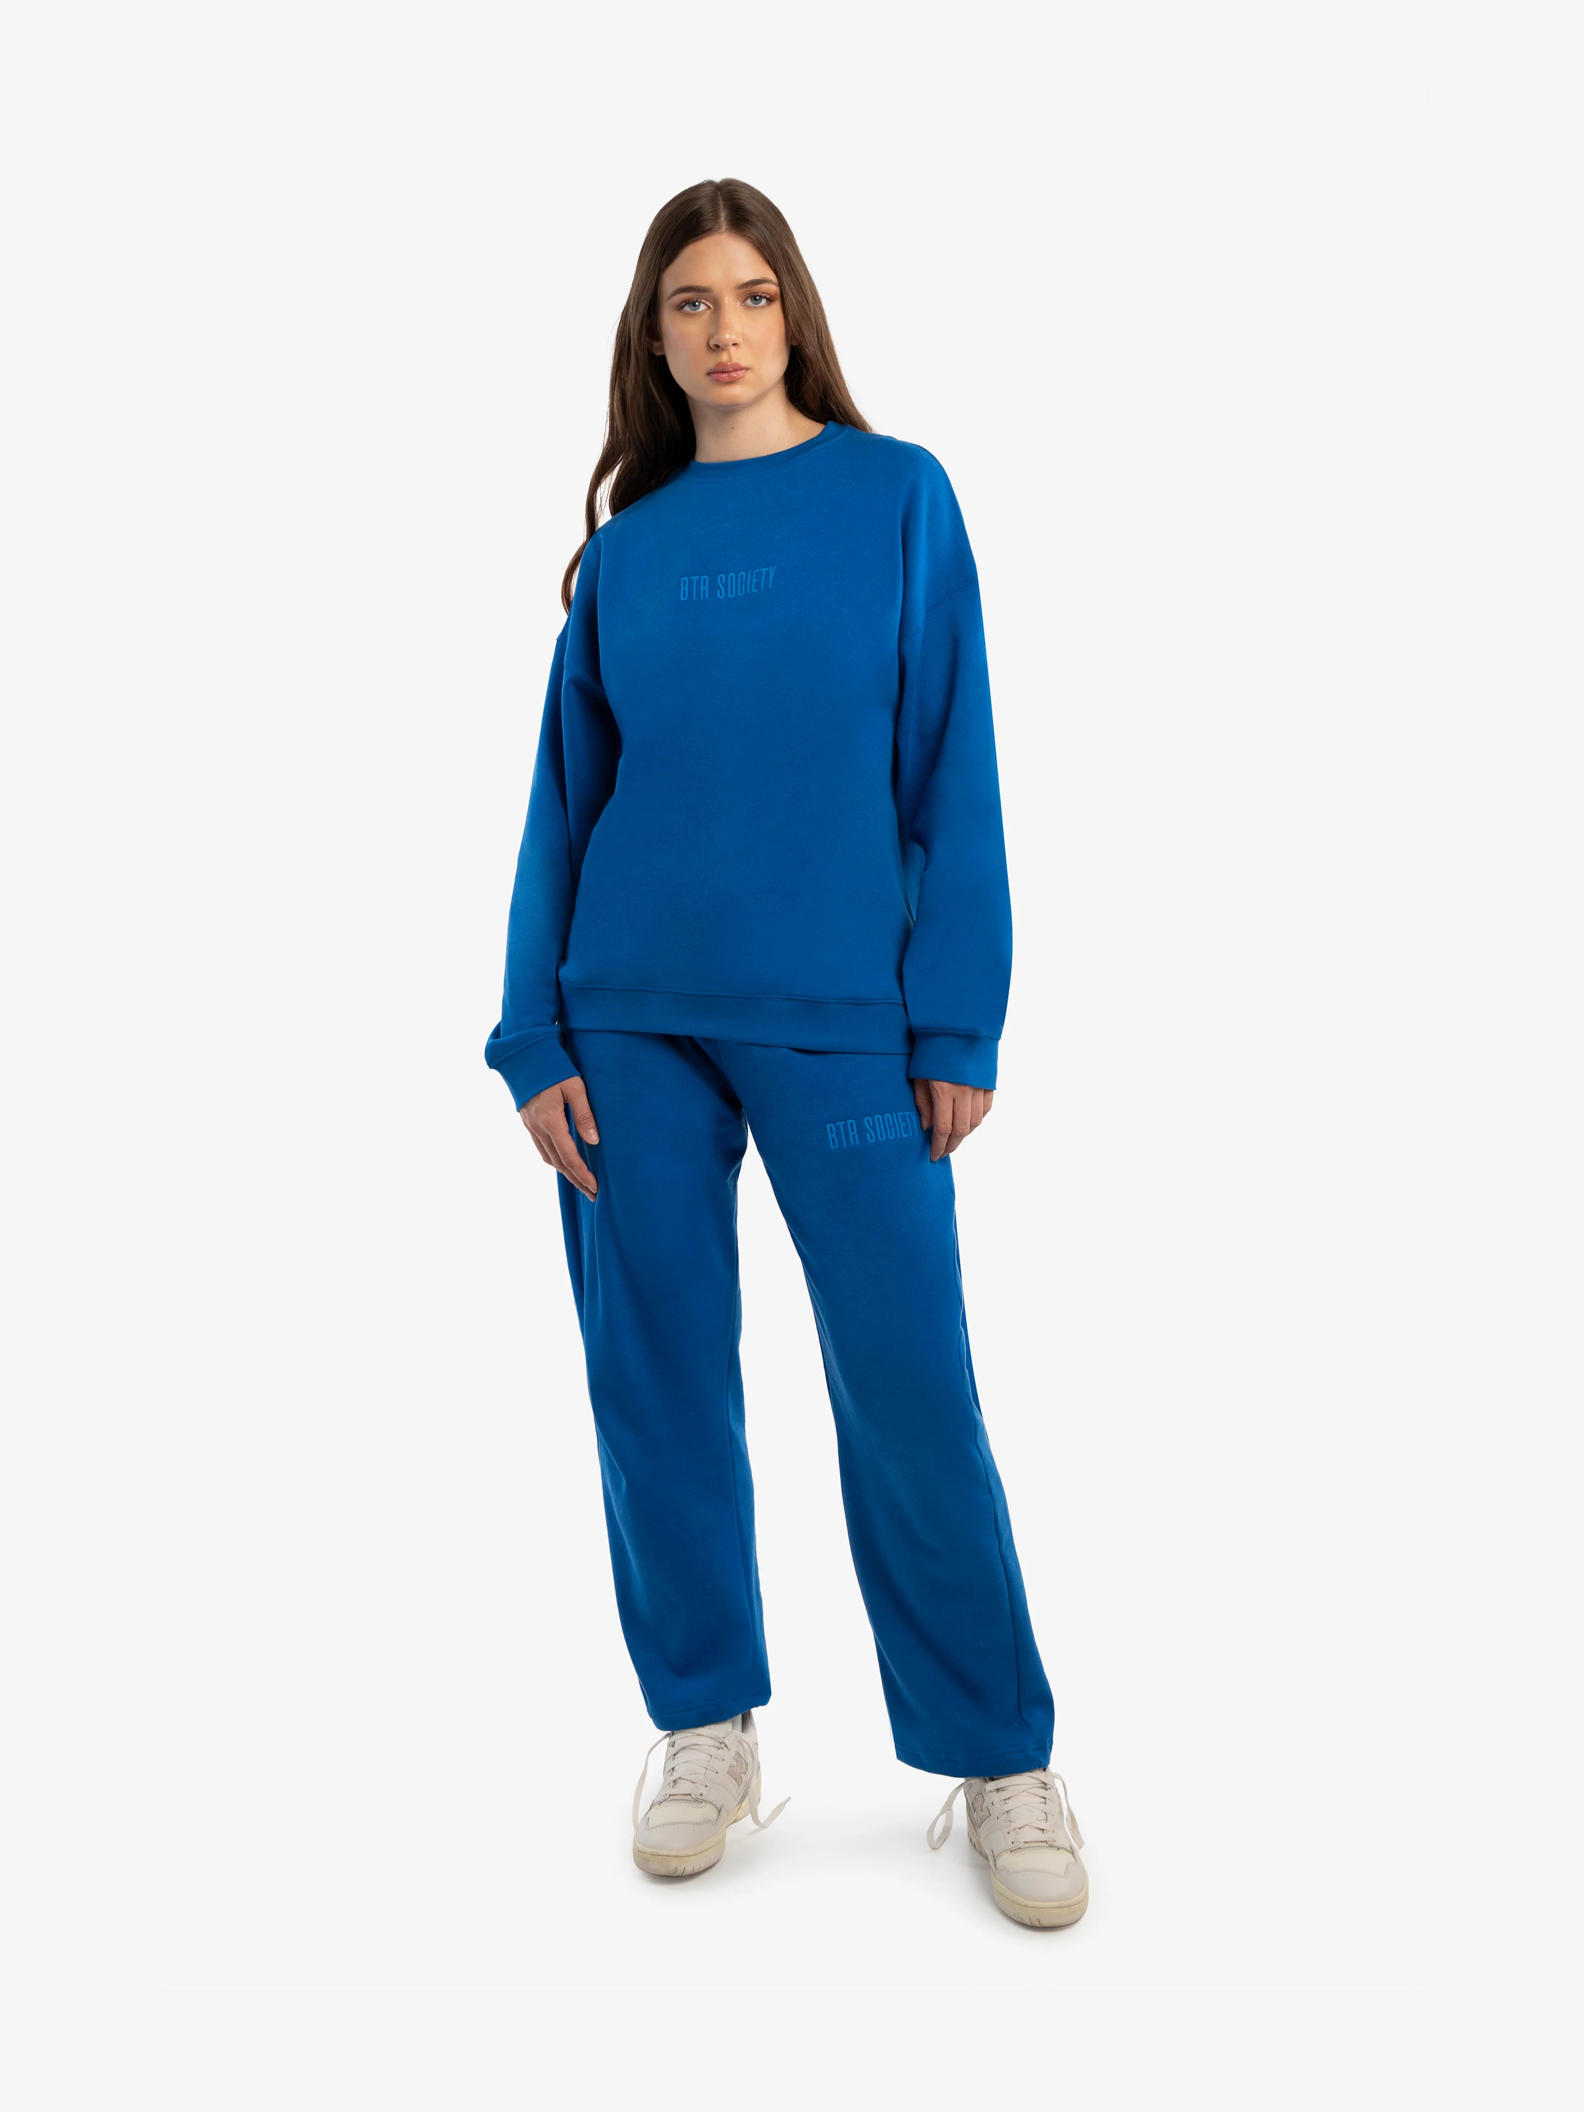
Ethically harvested certified organic cotton blended with elastane. Non-toxic GOTS certified eco-friendly dyes with natural breathability.
Get Catalog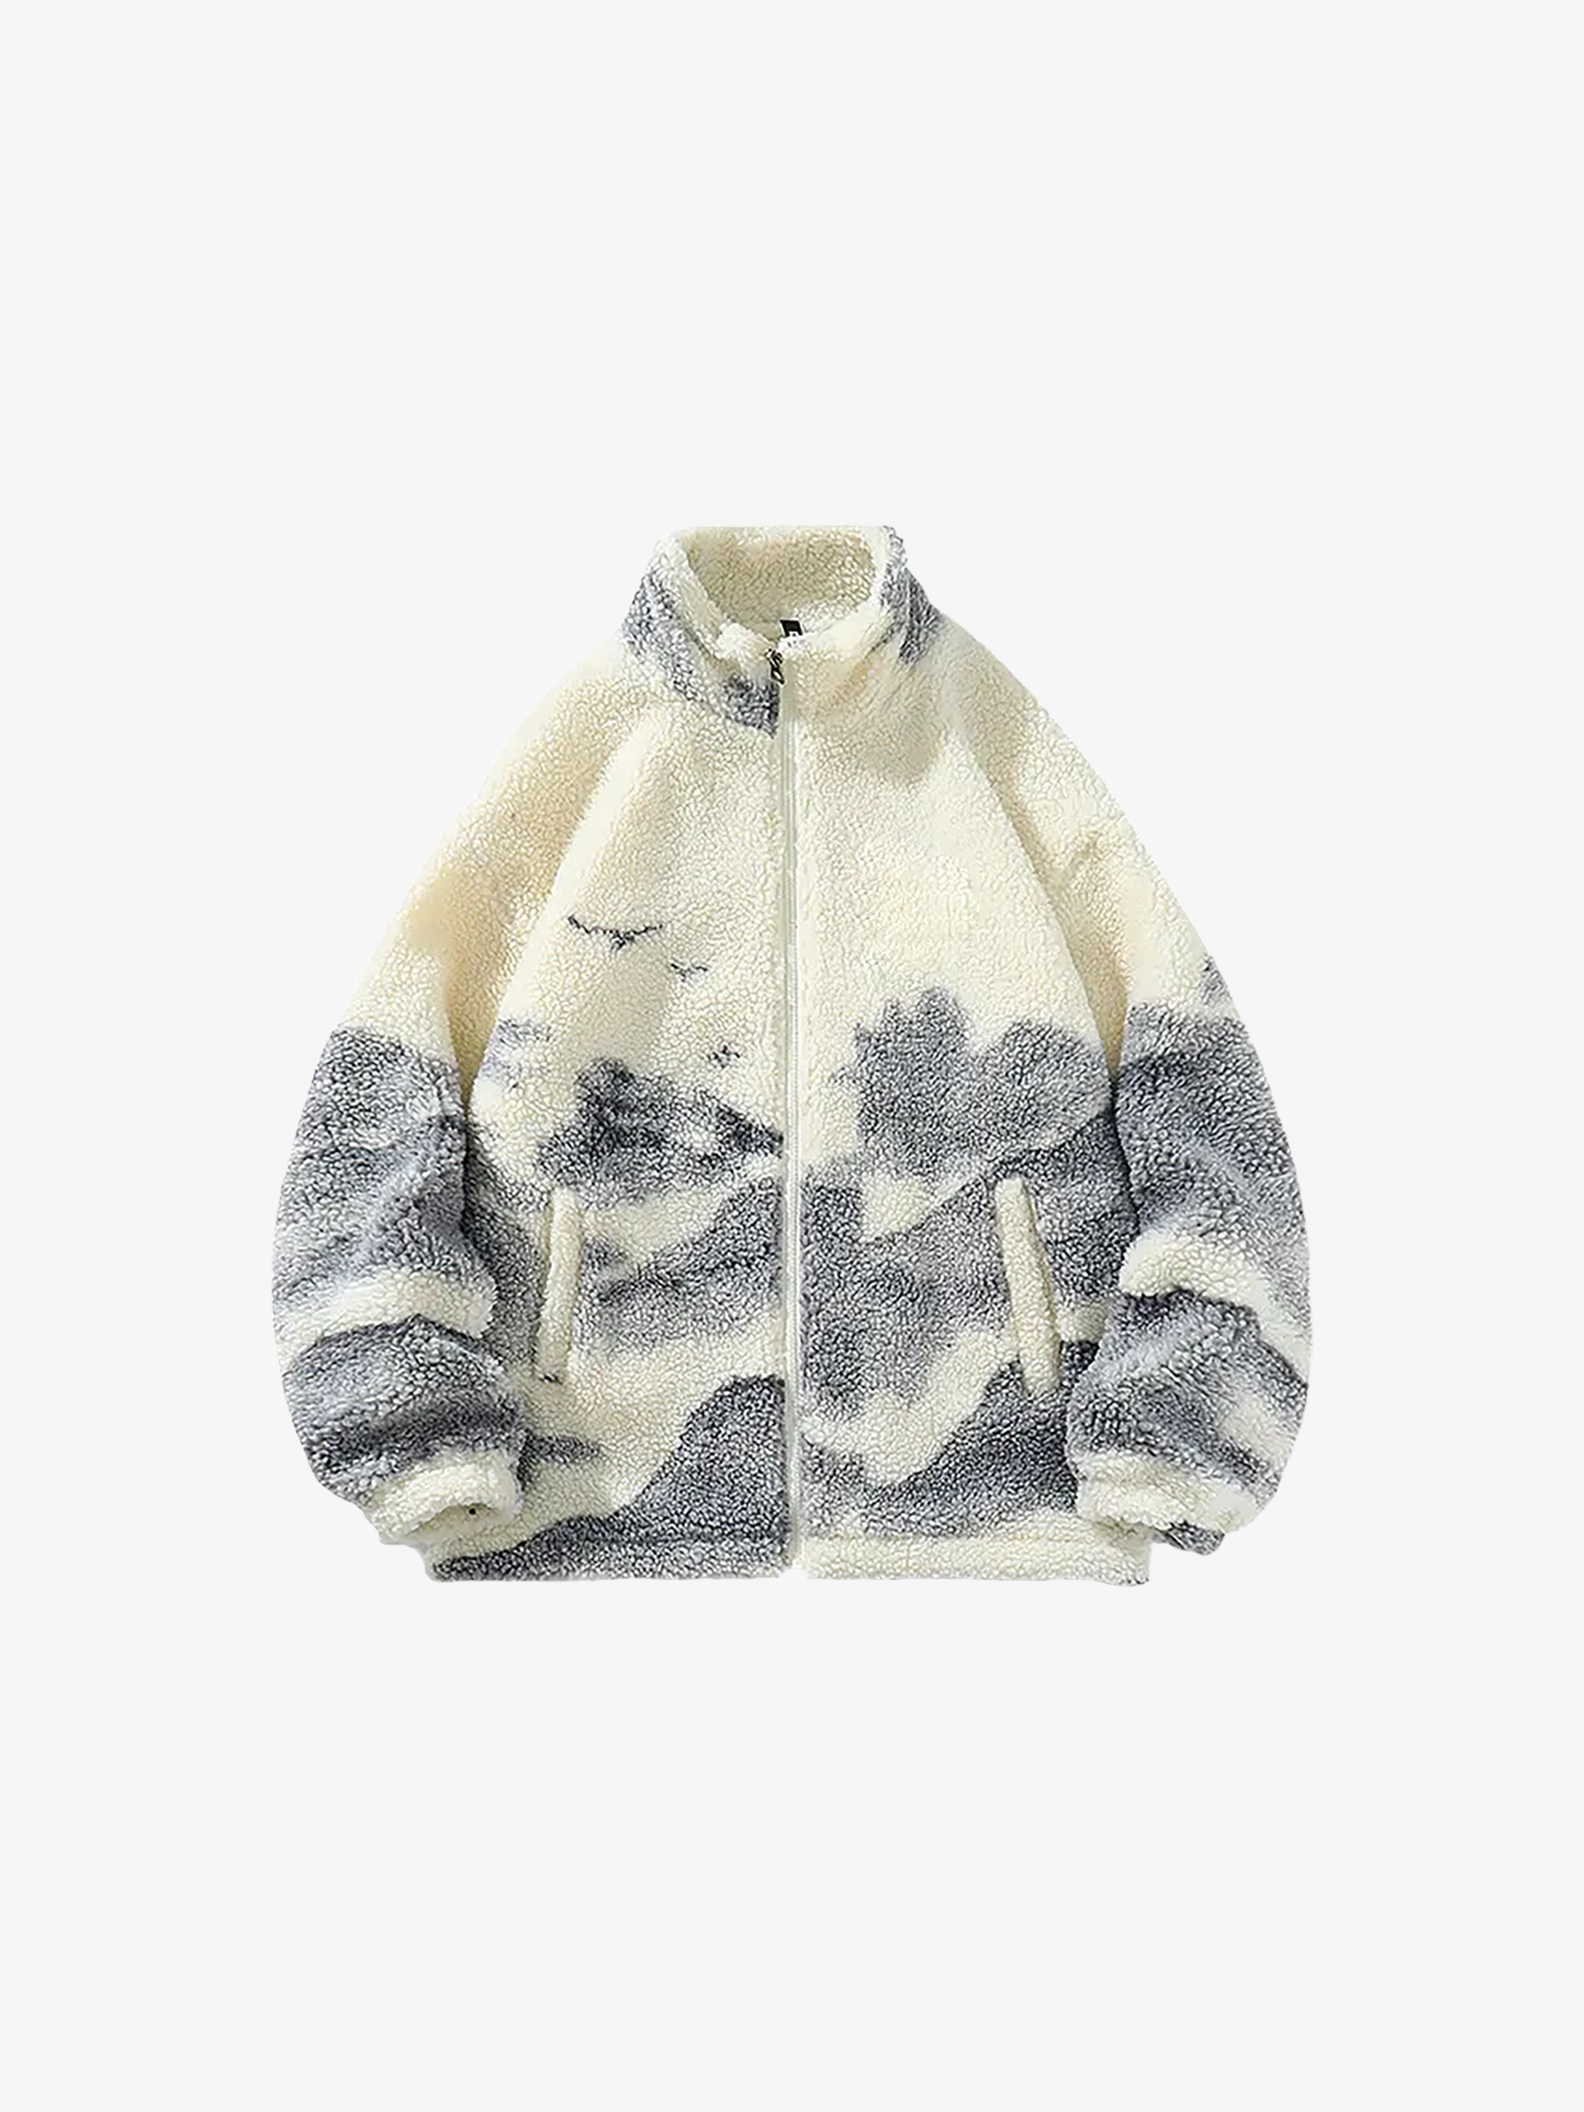
Custom engineered for New England outdoor runs and transitional climate studio visits. Lightly brushed back fabric for insulation without bulk.
Get Catalog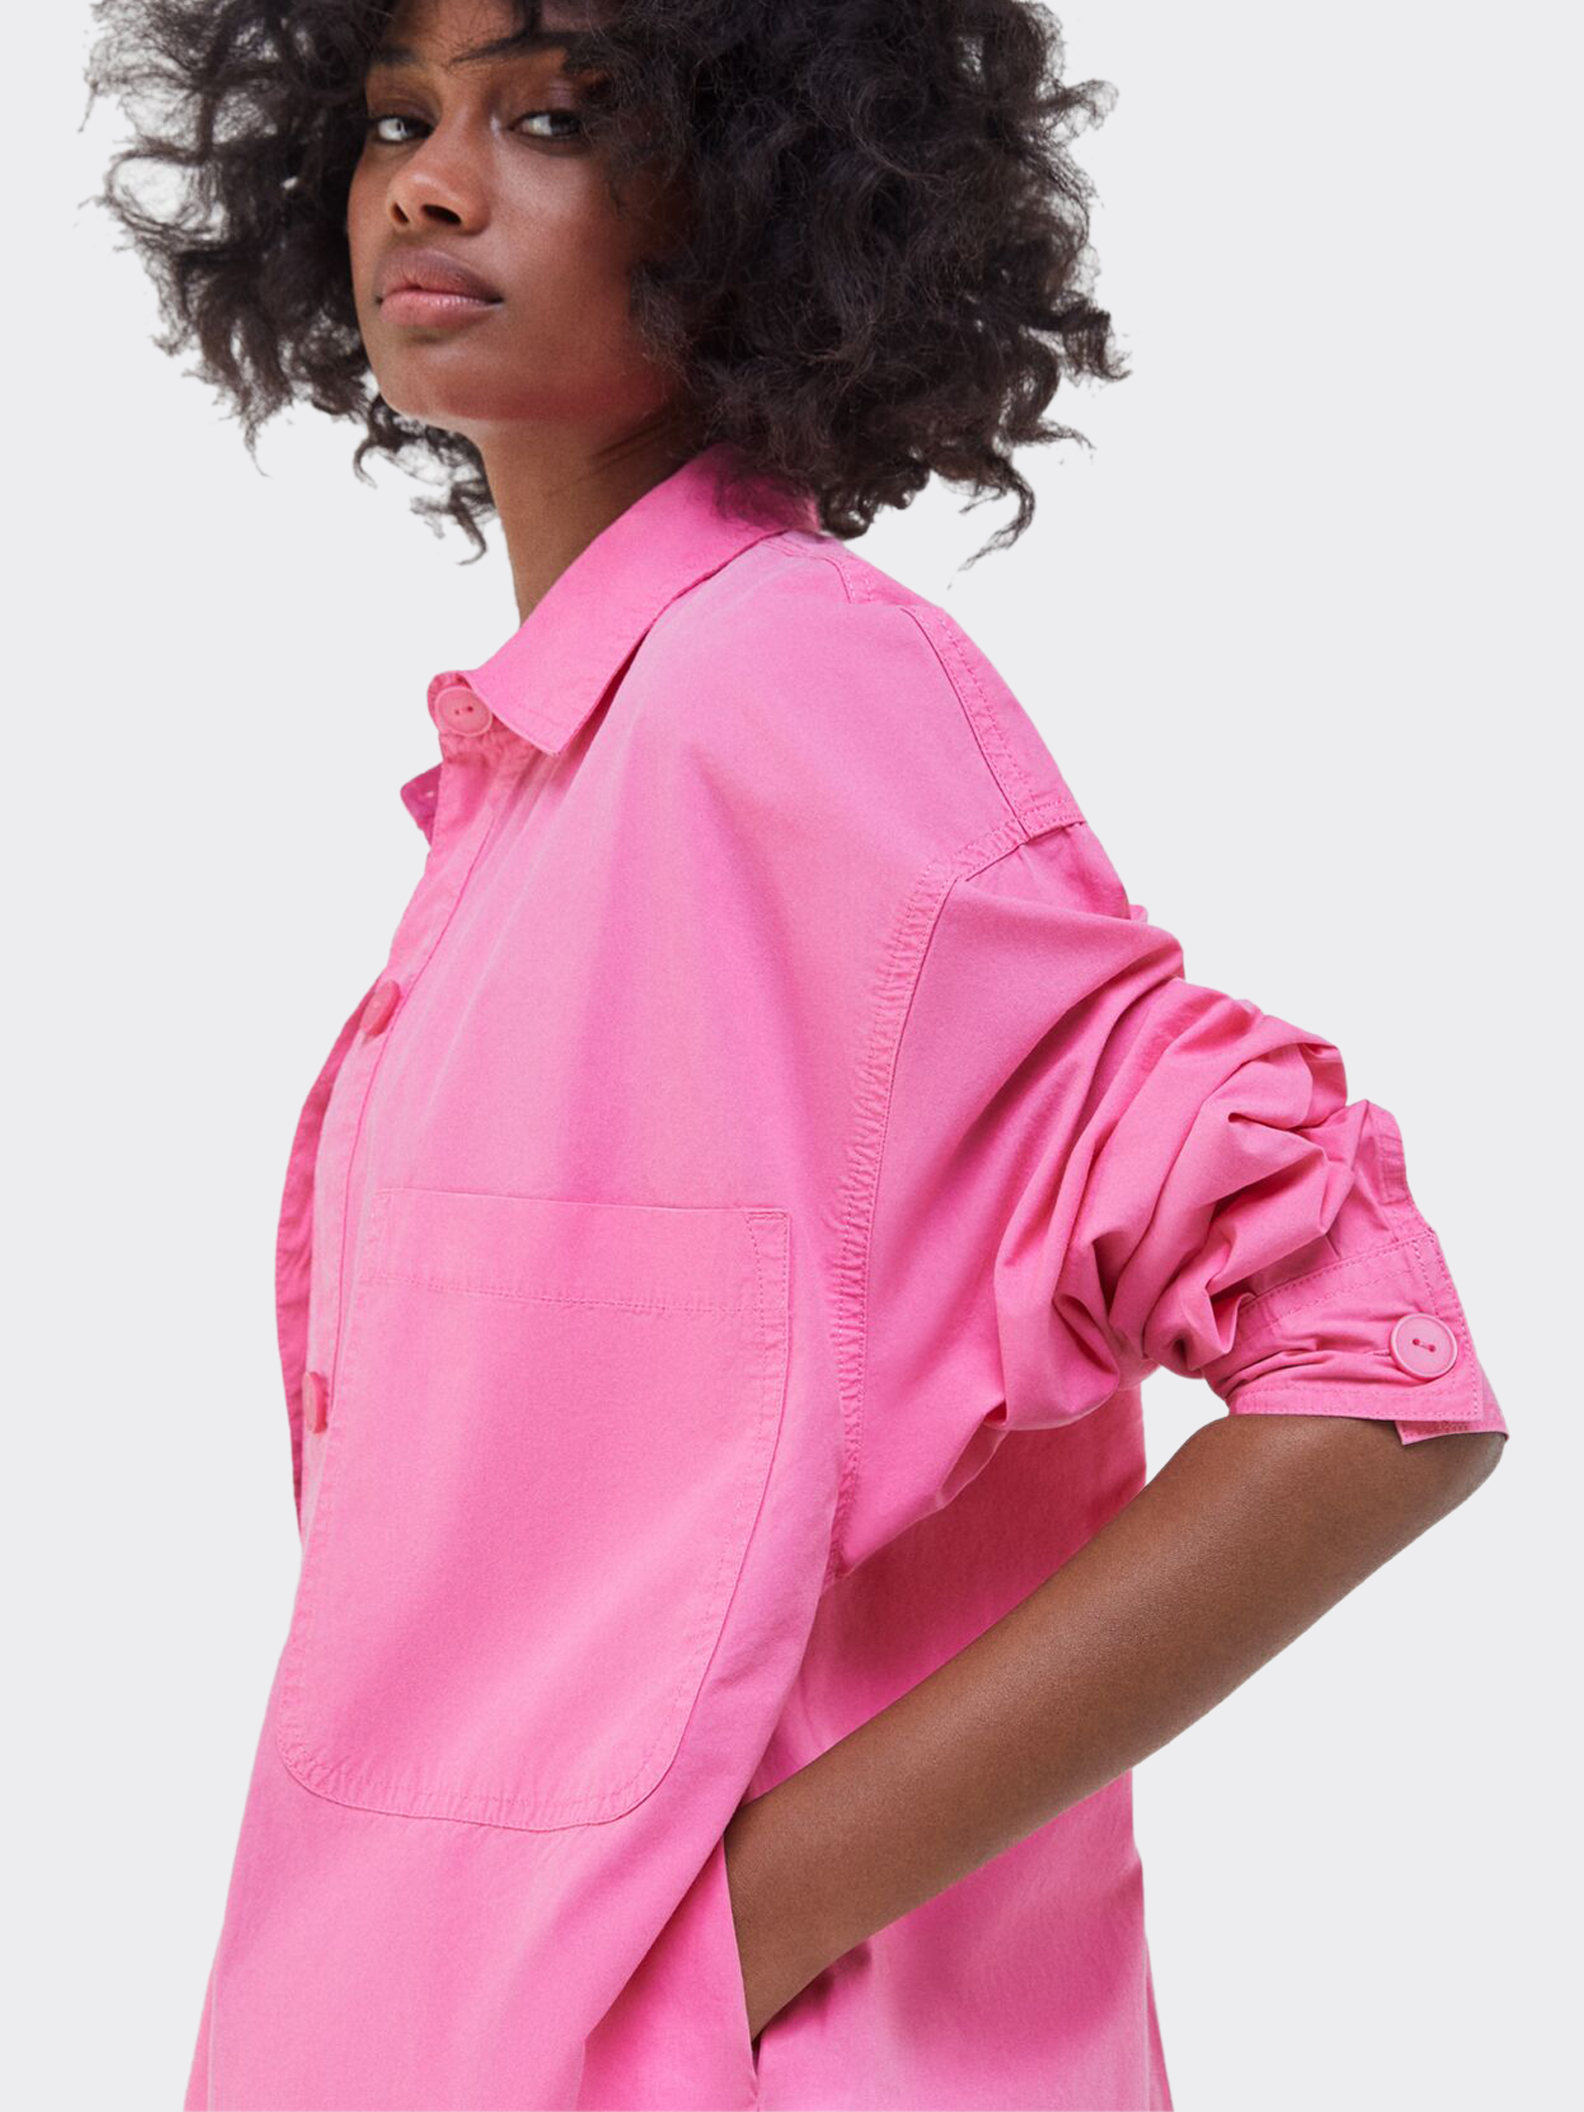
Precision laser-cut perforations at key heat zones for maximum air movement. Stitch-free bonded seams prevent chafing during prolonged wear.
Get Catalog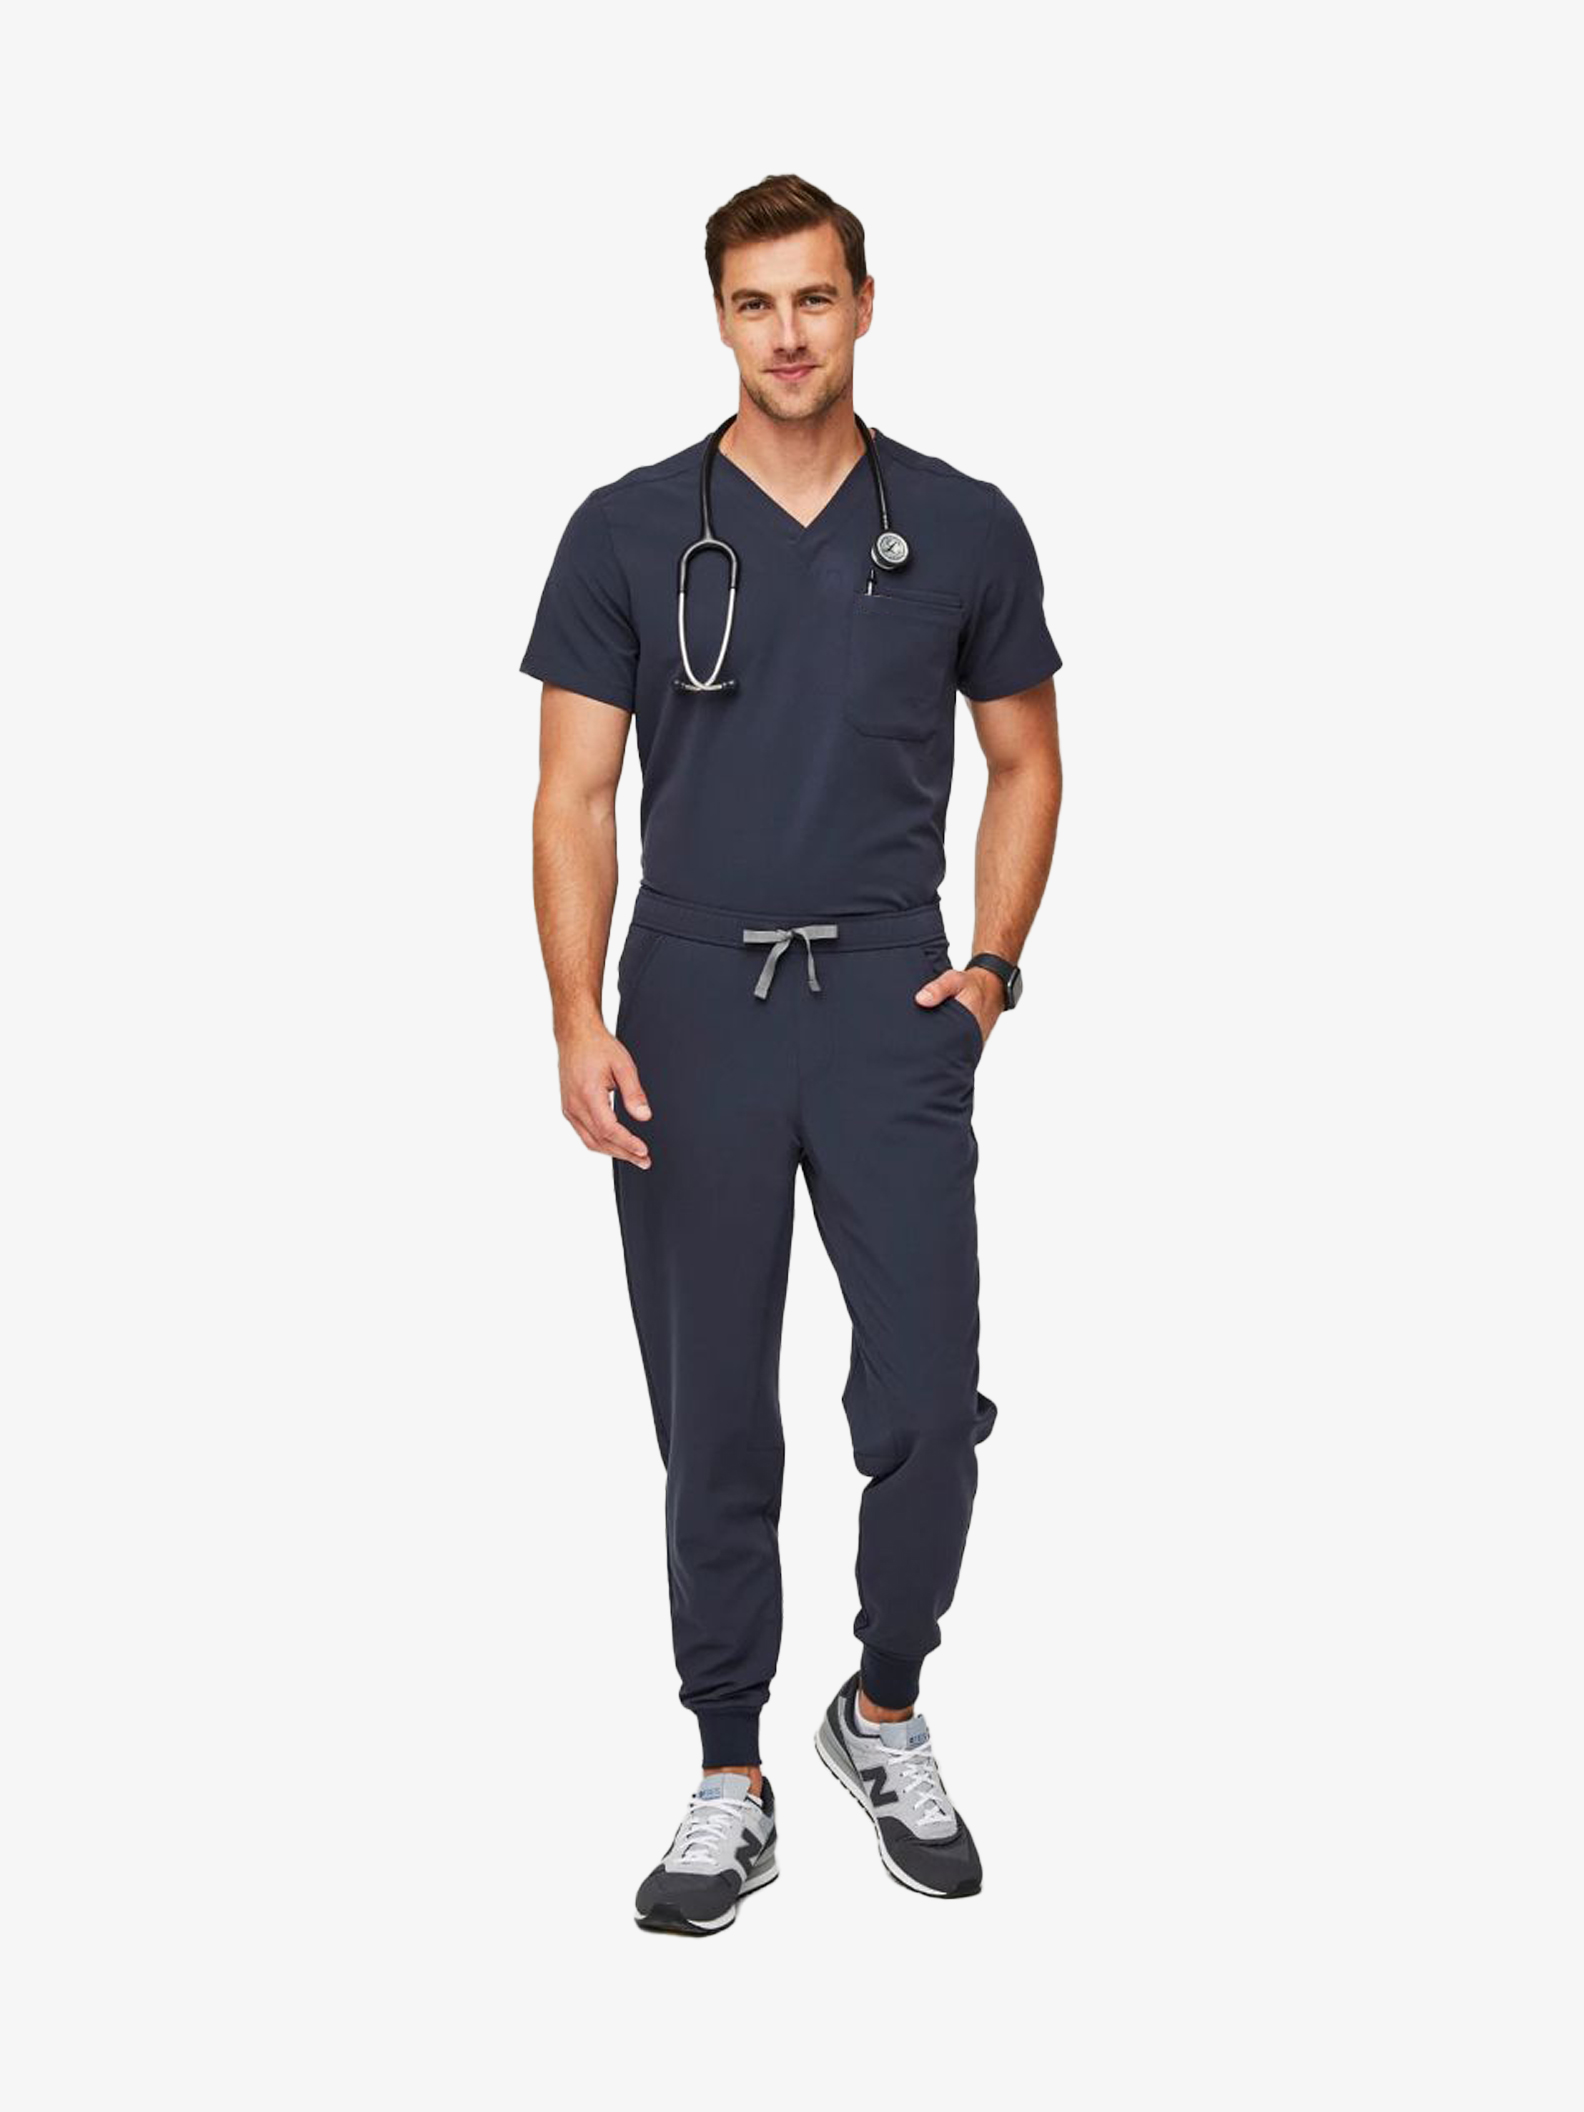
Constructed using rPET yarn treated with silver-ion antibacterial finish to eliminate odor-causing bacteria across intensive hot yoga sessions.
Get Catalog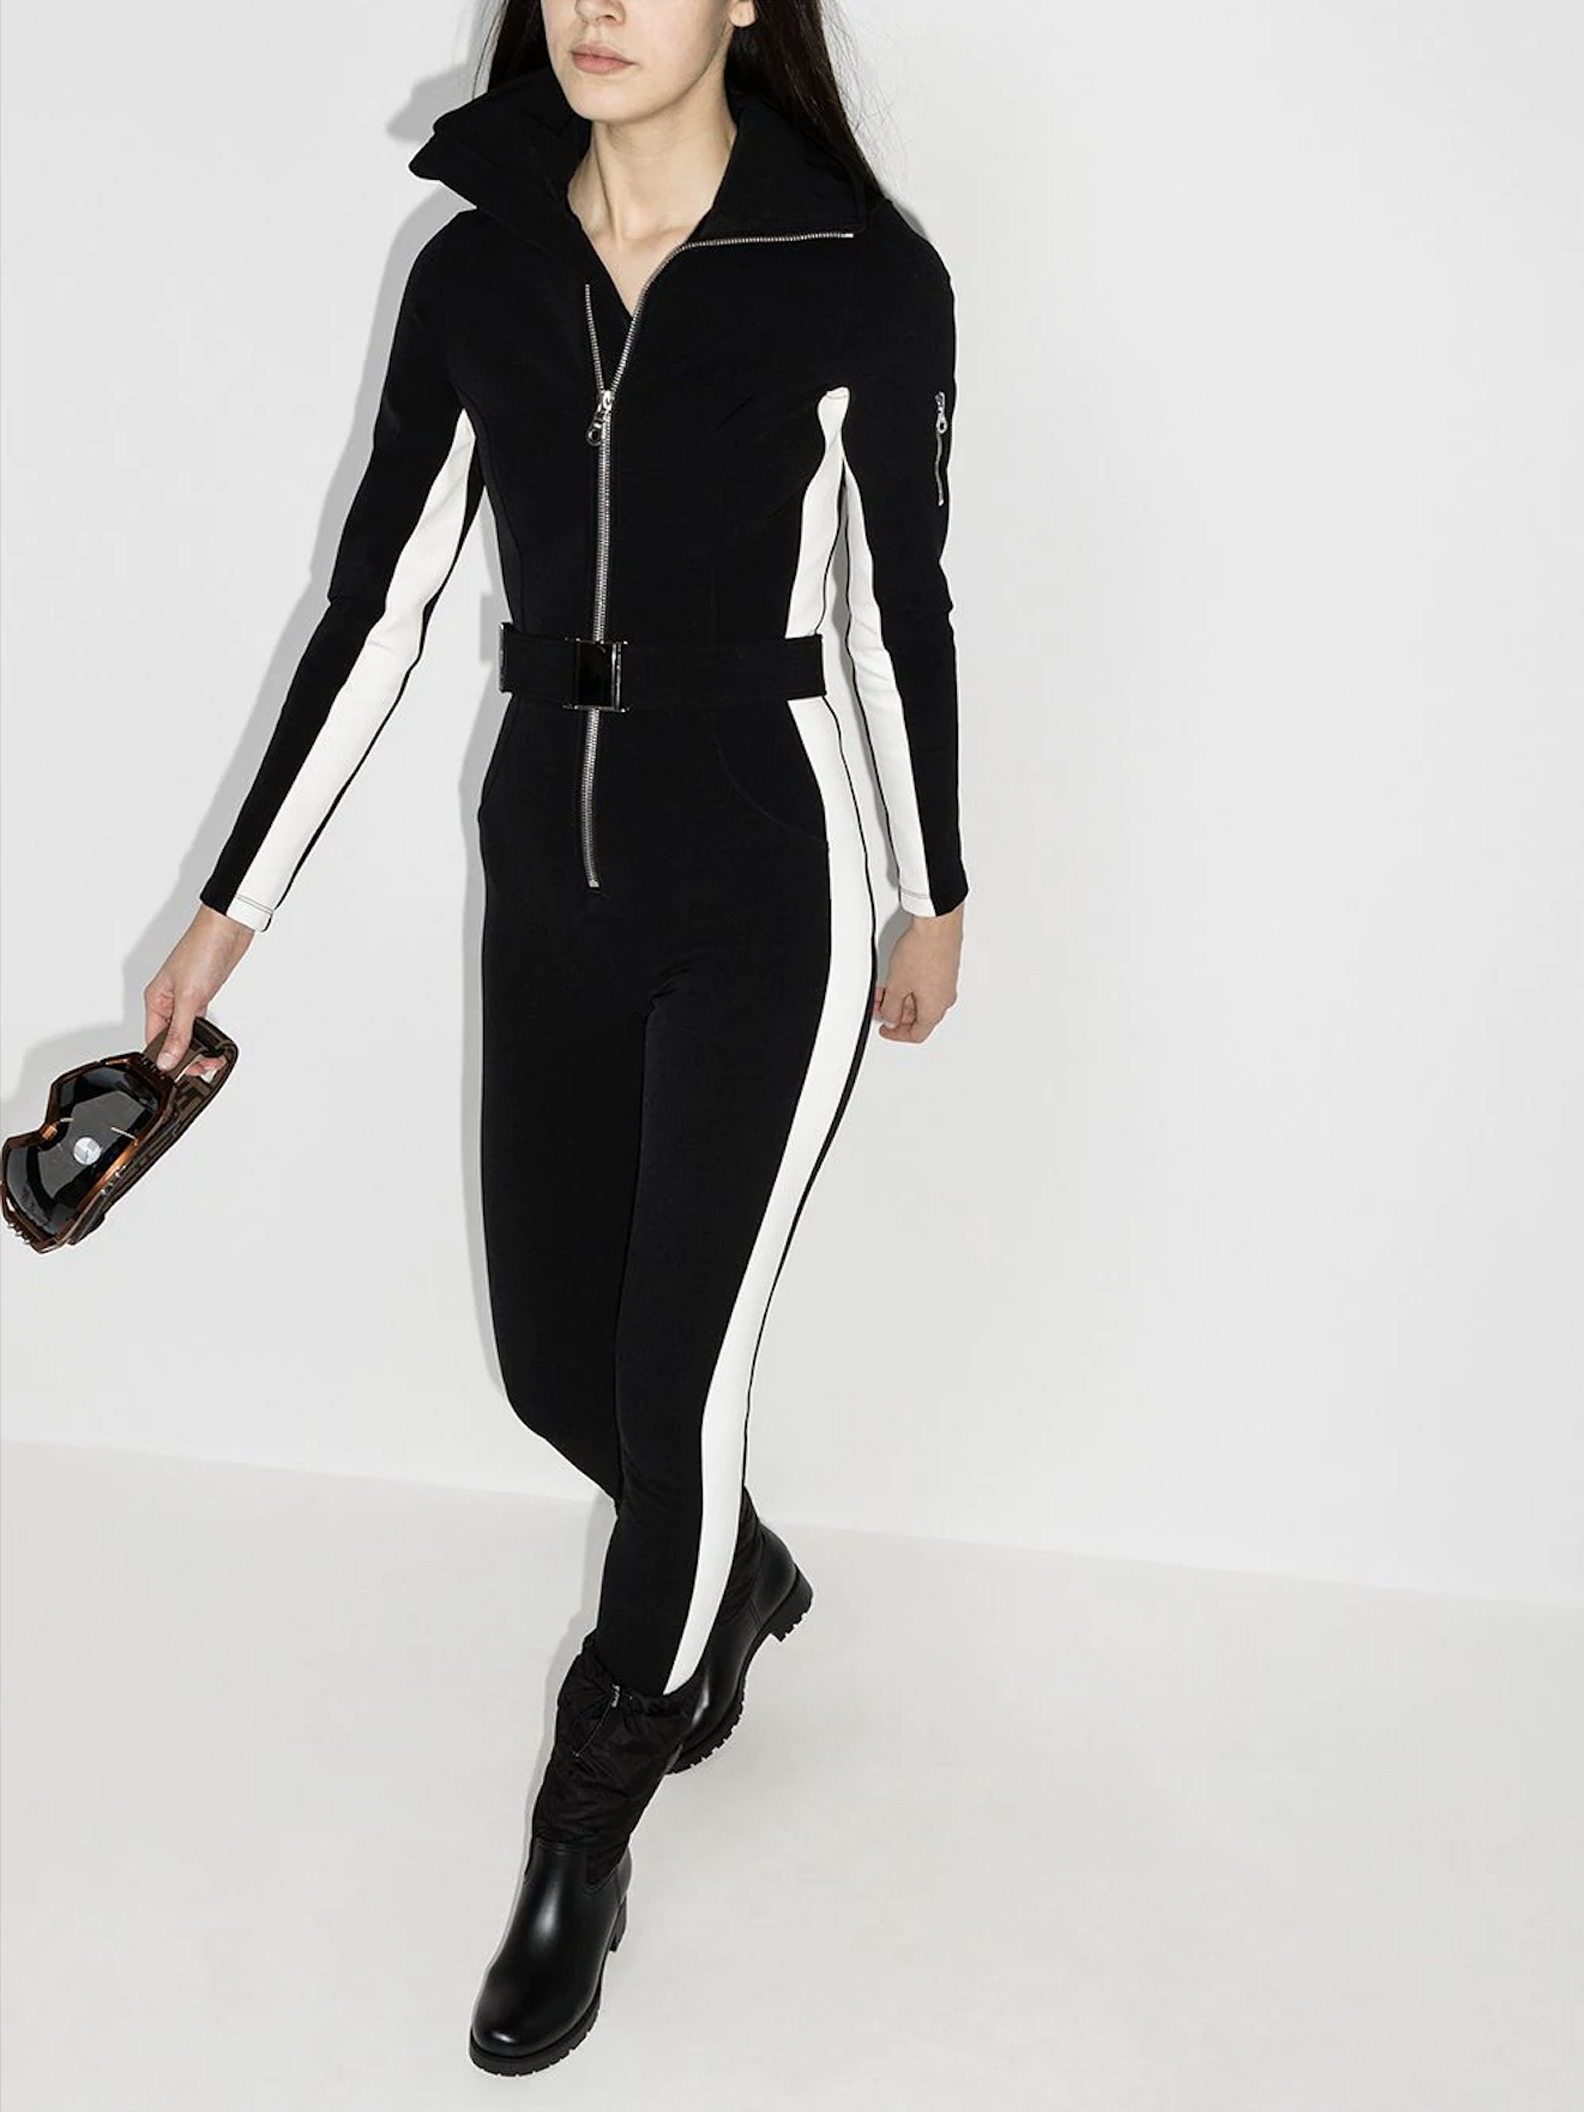
Ergonomic front zipper closure with interior security hooks. Designed for post-rehabilitation yoga, restorative fitness, and high-stability needs.
Get CatalogA comprehensive breakdown of fabric modulus, stretch recovery, seam integrity, and bust displacement management for commercial apparel buyers.
We utilize micro-filament Nylon 6.6 combined with premium elastane (Spandex/Lycra) in precise ratios ranging from 75/25 to 80/20. Nylon 6.6 provides superior tensile strength, chemical stability, and silk-like hand-feel compared to standard polyester, ensuring long-term shape retention despite repetitive laundering.
Unlike standard single-jersey knits, our dual-feed circular interlock knitting machines construct a balanced, non-see-through fabric architecture (240 GSM to 320 GSM). This guarantees complete opacity during deep squats and inversions while offering 360-degree uniform compression.
To eliminate friction-induced skin chafing during repetitive movement, all seams are constructed using 6-needle 4-thread ISO 607 flatlock stitching. Differential feed settings are dialed in per fabric blend to ensure seam stretch perfectly matches garment body elasticity.
In activewear garment manufacturing, mitigating Cooper’s ligament strain requires precise control over vector forces. Our design architecture incorporates localized inner-cup sling reinforcements, dual-layer power-mesh chest panels, and calibrated elastic underbust bands. By balancing vertical tension against lateral compression, our yoga sports bras reduce kinetic displacement by up to 68% during dynamic transitions (such as jump-throughs and Sun Salutations) without restricting diaphragmatic breathing capacity.
Vertically integrated production capabilities supplying brand owners in Boston, Massachusetts and across North America.
Understanding the distinct micro-climates, consumer demographics, and wellness trends across Massachusetts fitness hubs.
The Greater Boston athletic apparel market is driven by an educated, quality-conscious demographic that demands technical versatility. From high-end boutique studios in Back Bay and Newbury Street to high-density fitness spaces in the Seaport District and Cambridge, consumer expectations lean heavily toward apparel that performs under rigor and transitions seamlessly into street fashion.
Key strategic shifts adopted by East Coast fitness brands, apparel startups, and retail buyers in 2025/2026.
Boston-based apparel brands are increasingly bypassing trading agents and domestic middlemen to partner directly with vertically integrated mills. Direct factory engagement eliminates 20%–35% in cumulative margins, protects intellectual property, and ensures real-time oversight of tech packs, fabric lab dips, and bulk manufacturing schedules.
New England consumers actively audit brand ethics. Sourcing GOTS-certified organic cotton, Recycled Poly (GRS certified), and OEKO-TEX Standard 100 non-toxic dyes is no longer optional. Brands selling into Massachusetts retail channels require complete supply chain traceability documentation from raw yarn spinning down to final garment polybagging.
Boston lifestyle trends favor garment versatility. Yoga bras are now designed with bonded phone pockets, integrated headphone loops, and dual-purpose aesthetics suitable for rowing on the Charles, studio Pilates, and casual coffee meetings in Harvard Square.
To mitigate inventory overstock risks in fluctuating retail climates, Boston brands prioritize manufacturers offering moderate starting MOQs (300 pieces per style) alongside the infrastructure to seamlessly scale into 50,000+ unit repeat orders upon market validation.
Over four decades of export mastery, delivering custom athletic apparel directly from our Ludhiana facility to Boston buyers.
We manufacture our own knitted fabrics. From custom GSM weight target adjustments to proprietary nylon-spandex blends, we control fabric hand-feel, stretch modulus, and color matching in-house.
Your tech packs, artwork, CAD pattern blocks, and brand assets remain strictly confidential inside our facility. We never sub-contract your production or shop your designs to third parties.
Incorporate active performance finishes including moisture-wicking dry-fit, silver-ion antimicrobial anti-odor treatment, UPF 50+ UV shielding, and soft-touch peached/brushed surface finishes.
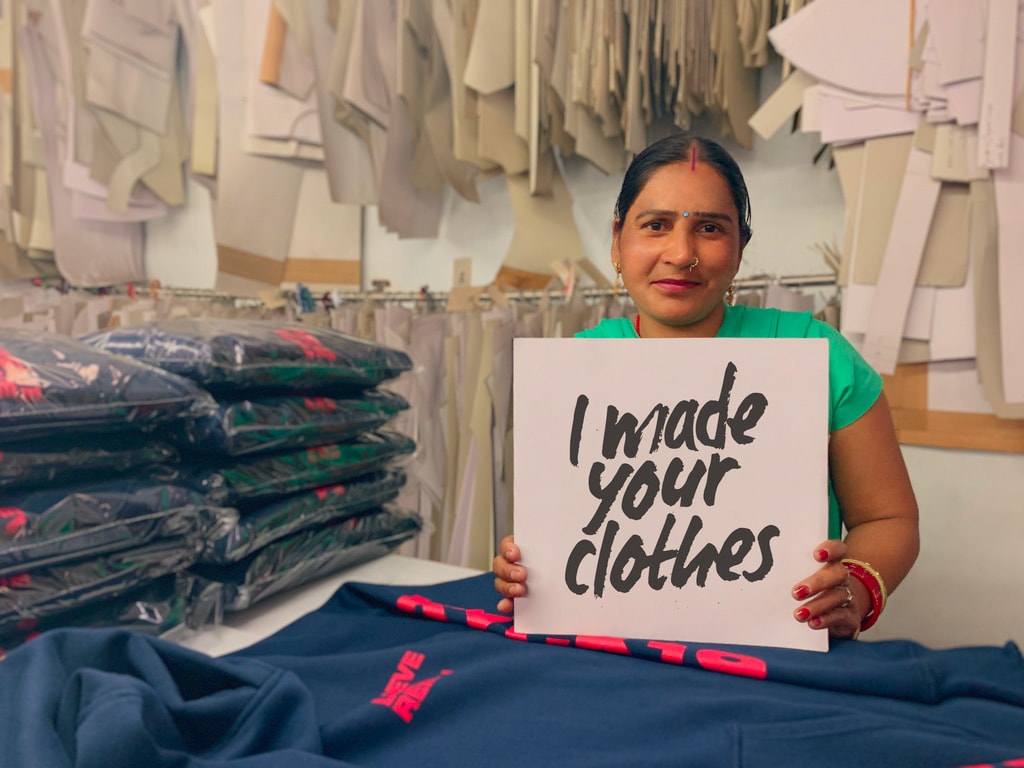
Our factory operates under fair trade labor standards: fair living wages, documented working hours, safe ergonomic environments, and a high ratio of skilled female pattern masters and stitchers.
Bespoke silicone grip prints, reflective heat-transfer logos, woven jacquard underbust elastics, nickel-free metal sliders, and customized eco-friendly retail packaging built to your exact specs.
Seamless customs clearance handling and direct air/sea freight shipping straight to your distribution centers in Greater Boston, Logan International Airport hub, or Port of Boston terminals.
Everything brand managers, procurement directors, and activewear founders need to know before issuing a purchase order.
Partner directly with an established custom apparel manufacturer. Request our technical product catalog, fabric swatch cards, and instant wholesale pricing today.